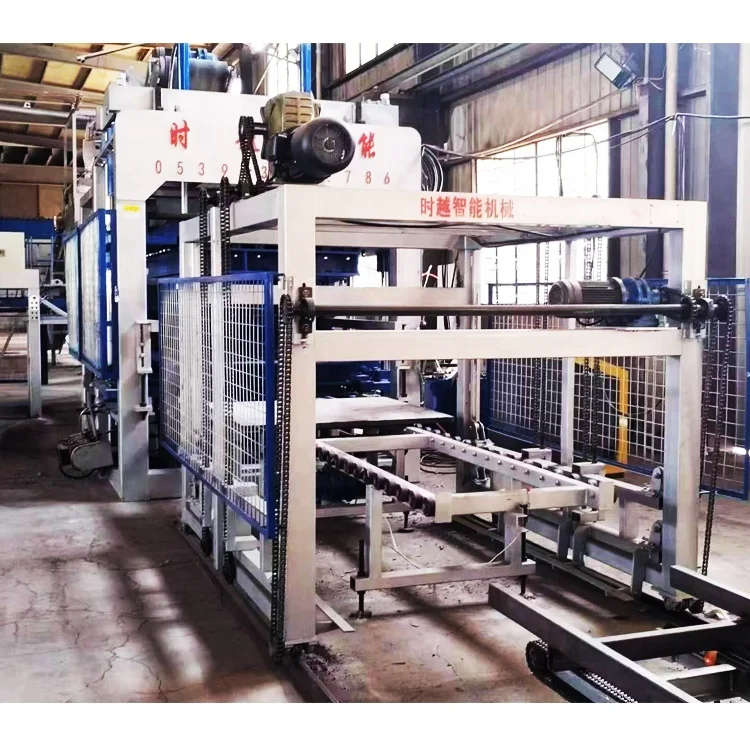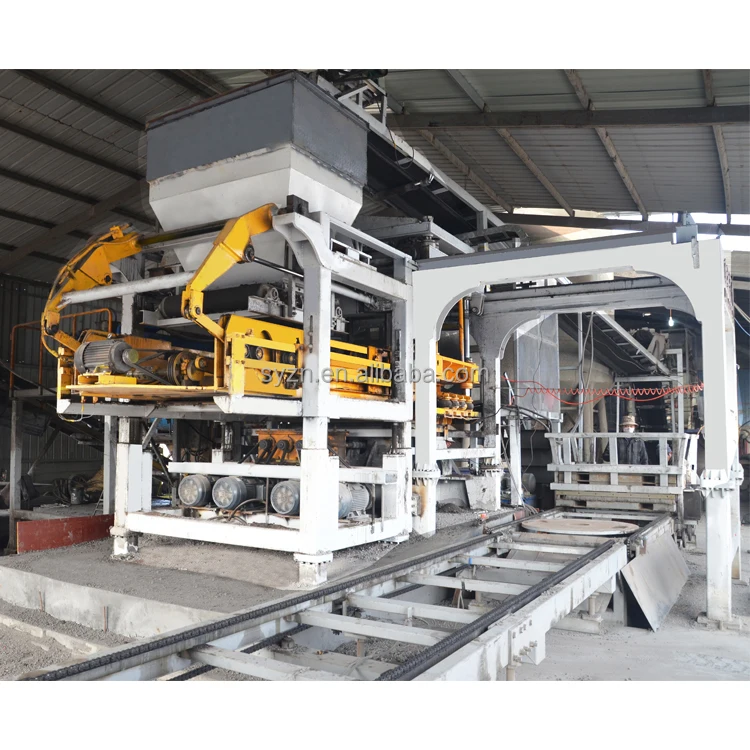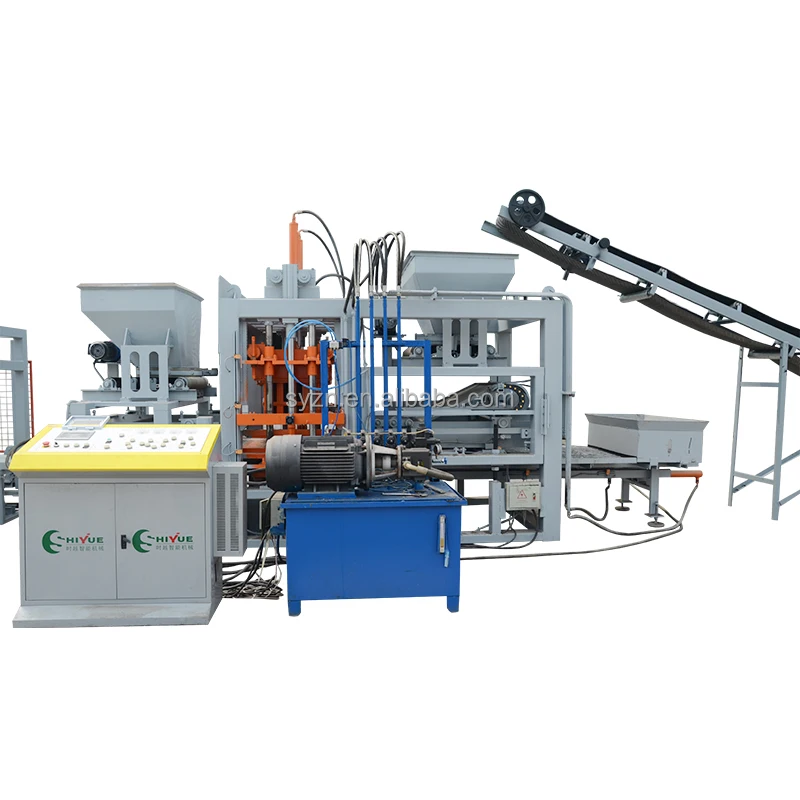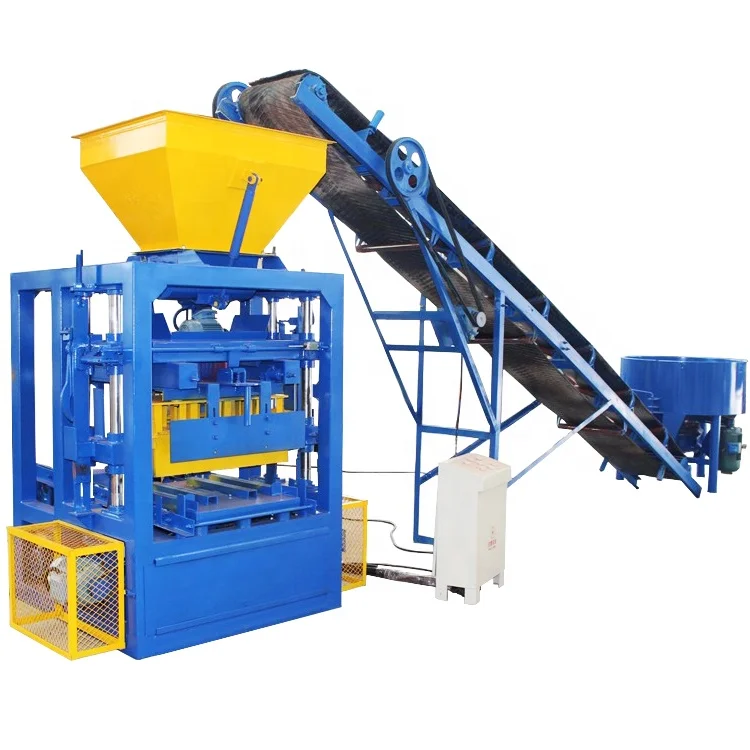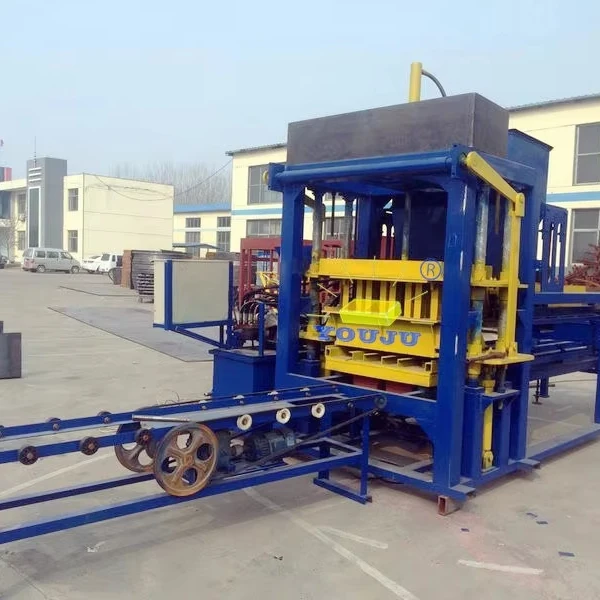
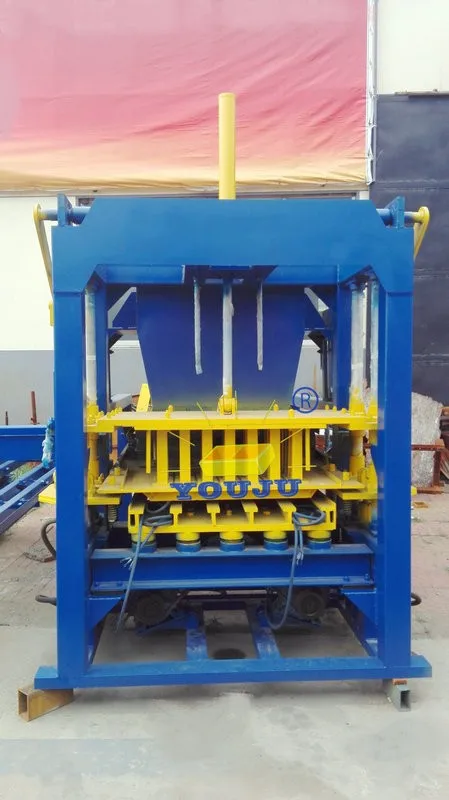
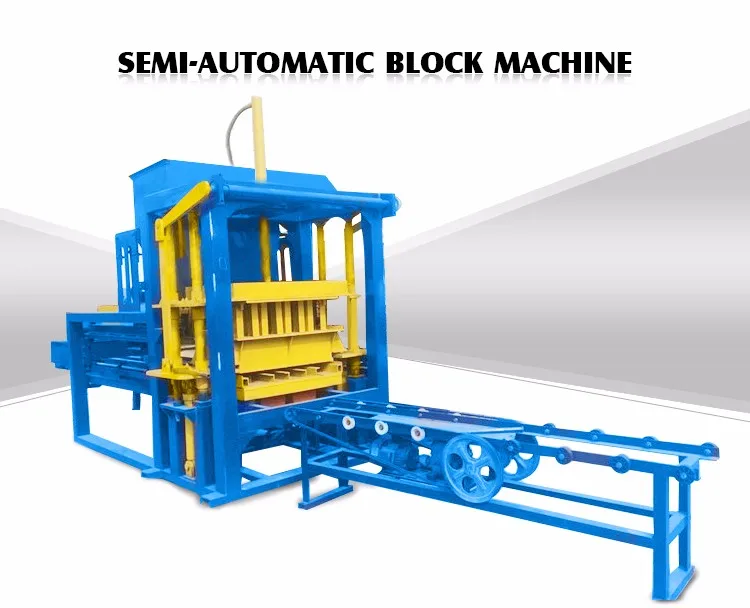
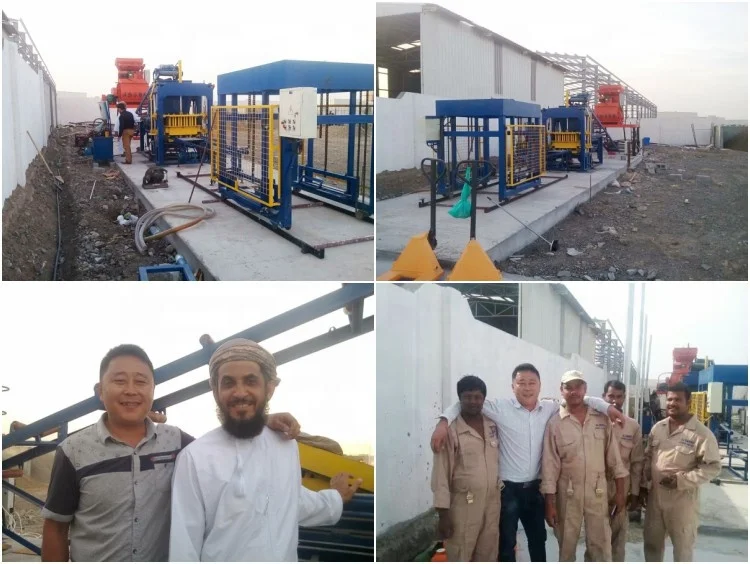
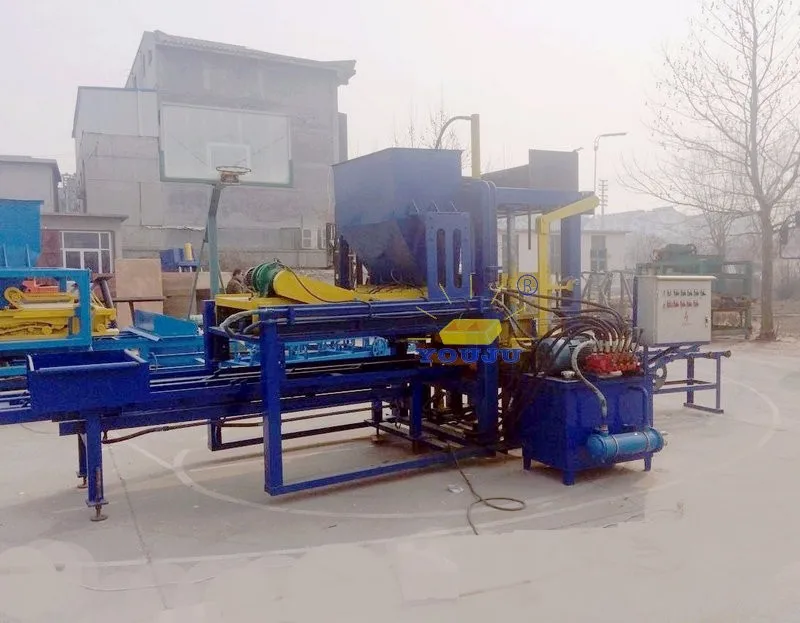
Description
Matched System Specification — every output figure for the QT4-20 is tied to a specific block format and cycle time, eliminating the guesswork that leaves plants running below expectation.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-20 |
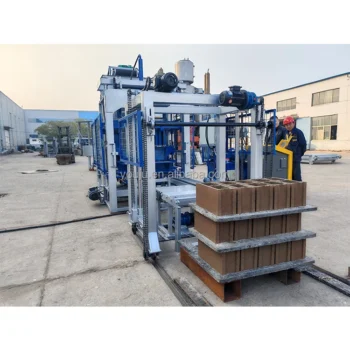
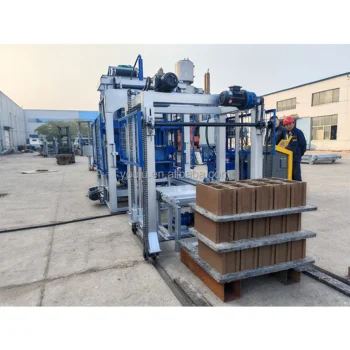
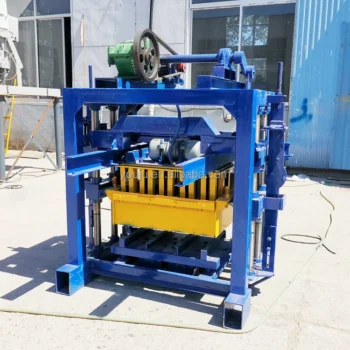
| Product Type | Fully Automatic Hydraulic Block Making Machine |
| Overall Dimensions (L×W×H) | 7100×1600×2610 mm |
| Net Weight | 5 T |
| Rated Power | 27.5 kW |
| Hydraulic Pressure | 16–21 MPa |
| Vibration Form | Platform Vibration |
| Vibration Frequency | 4600 r/min |
| Vibration Force | 40 kN |
| Moulding Area | 400×800 mm |
| Pallet Size | 1020×570 mm |
| Cycle Time | 15–25 s (basis to be confirmed by block format and material) |
| Demolding Method | Hydraulic |
| Control System | PLC (fully automatic) |
| Recommended Factory Area | 500 m² |
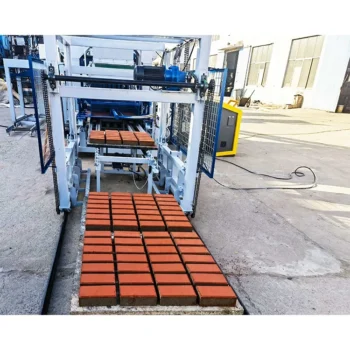
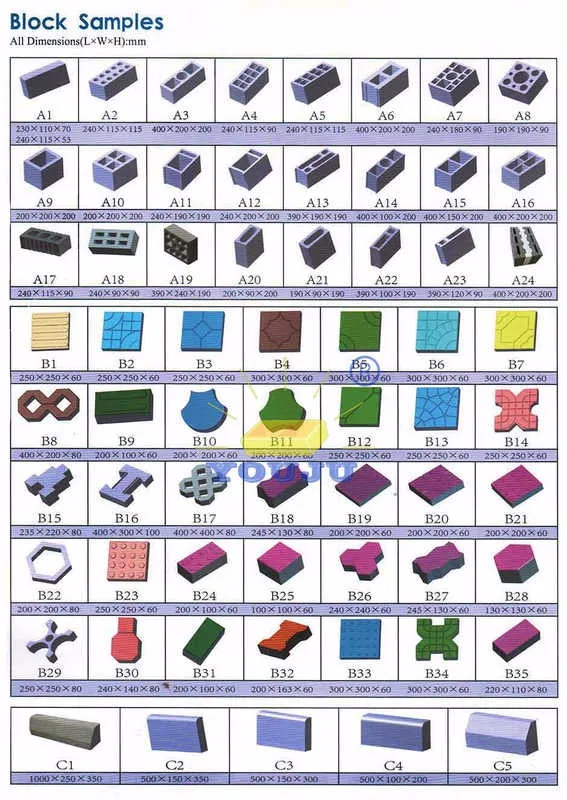
| Applied Products | Concrete blocks, hollow/solid blocks, pavers |
| Raw Materials | Crushed stone, sand, cement, fly ash, gravel, slag |
| Output Capacity (Hollow brick 400×200×200 mm, 4 pcs/mould) | 7,200–9,600 pcs/day (based on 15–20 s cycle) |
| Output Capacity (Porous brick 240×115×90 mm, 14 pcs/mould) | 20,200–26,800 pcs/day (based on 15–20 s cycle) |
| Output Capacity (Standard brick 240×115×53 mm, 28 pcs/mould) | 47,400–53,700 pcs/day (based on 15–17 s cycle) |
| Warranty | One year for the whole machine |
Application Suitability
| Application | Material or Output |
|---|---|
| Stationary hollow block plant for regional building supply | Crushed stone, sand, and cement producing 400×200×200 mm hollow blocks, 4 pcs per mould |
| Paver and kerbstone production for municipal contractors | Gravel and fly ash mixes on 1020×570 mm pallets |
| Solid and porous brick line for housing developments | Cement and sand blends producing 240×115×90 mm porous bricks, 14 pcs per mould |
| Standard brick manufacturing for masonry projects | Local aggregate and cement yielding 240×115×53 mm bricks, 28 pcs per mould |
| On-site concrete product fabrication by construction firms | Slag and dust blends for mixed-format production on a single pallet system |
What "7,200 Pieces Per Day" Actually Means for Your Hollow Block Line
Every capacity figure here is anchored to a named block format and a measured cycle range — not a single headline number.
When I first started on the assembly floor, buyers would call asking why their block machine never hit the brochure output. The answer was almost always the same: the quoted number assumed a standard hollow block, but the plant was running pavers or porous bricks with longer press cycles and slower demolding. The QT4-20 block machine specifications list three distinct daily outputs because each format demands its own press time, vibration duration, and hydraulic stroke sequence. A technical buyer sizing a fully automatic hollow brick production line needs to know which number applies to the product the local market actually buys, not which number looks best on a comparison sheet [NEED_CITE: block format impact on cycle time and daily throughput].
Matching Vibration Force to Your Local Aggregate
The 40 kN platform vibration at 4600 r/min works well with well-graded river sand and crushed limestone, but volcanic scoria or high-clay-content gravel absorbs energy differently. When the mix design does not match the vibration profile, block density drops and surfaces crack during demolding. Before we configure the QT4-20 block machine specifications for your line, we ask you to send a sample of your actual aggregate so we can run test cycles and confirm the pressure-to-vibration balance.
Pallet Size, Curing Area, and the Forklift You Already Own
The 1020×570 mm pallet determines how many blocks travel through the press per cycle, but it also has to fit your curing racks and the fork dimensions of the forklift on site. A fully automatic hollow brick production line is only as fast as its slowest station, and if the pallet cannot be retrieved from the curing area quickly enough, the press sits idle. We confirm pallet material — hardwood, bamboo-composite, or steel — against your humidity and curing duration before the machine enters production [NEED_CITE: pallet material selection and curing environment].
Reading the Specs That Matter for Block Density
Hydraulic pressure between 16 and 21 MPa combined with 40 kN vibration force determines the compactness of each block. Higher pressure alone does not guarantee strength; the vibration must distribute force evenly through the mould cavity so the mix settles without voids. The 400×800 mm moulding area sets the maximum footprint per cycle, meaning a larger paver will consume the full area while standard bricks tile across it, affecting how you plan daily format changes. The 15–25 s cycle range reflects the difference between a thin standard brick that demolds quickly and a deep hollow block that needs extended vibration to fill the core cavities. The 27.5 kW rated power must be supported by a dedicated circuit with the correct voltage and frequency — details we confirm in writing before the PLC is programmed, because reprogramming a controller after arrival delays commissioning by weeks [NEED_CITE: voltage and frequency standards by export market].
The Cost of Skipping the Mix-Design Conversation
A buyer in East Africa once received a machine configured for quartz sand, then tried to run it on lightweight pumice without adjusting the hydraulic pressure or vibration frequency. Blocks crumbled at the stacker, and by the time the issue was diagnosed, three weeks of production had been lost. The problem was not the QT4-20 — it was that nobody asked what aggregate would actually feed the hopper. When vibration force and mix design are mismatched, you spend more on cement to compensate for weak blocks, and the extra cement changes the water demand, creating a cascade of adjustments that operators cannot keep up with [NEED_CITE: aggregate variability effects on concrete block compressive strength].
Why Source the QT4-20 Here
The QT4-20 block machine specifications are not pulled from a catalogue default — they are set against your target block format, local raw material, and existing plant layout. Mould design covers the exact formats your regional market demands, with custom drawings available when standard options do not match. Pallet size and material are confirmed alongside your curing rack dimensions and forklift capacity, so the line moves as one continuous flow rather than bottlenecking at retrieval. Automation level is selectable: a buyer can start with manual pallet handling and add automatic stacking later without replacing the press. Voltage, frequency, and PLC display language are documented and agreed before production begins, removing the most common cause of delayed commissioning.
Documentation & Verification
- Line layout drawing with capacity calculation for each quoted block format
- Mould drawing and format list confirming producible dimensions on the 400×800 mm area
- Voltage, frequency, and PLC language confirmation sheet signed before production
- Factory test record on your specific aggregate and mix design before dispatch
- Hydraulic and electrical schematic matching the as-built 16–21 MPa system
- Wear parts and mould catalogue with part numbers for first-year replacements
Installation, Commissioning & Support
- Foundation plan based on the 7100×1600 mm footprint and 5 T operating weight
- Dedicated power circuit sized for the 27.5 kW rated load at your confirmed voltage
- PLC parameter tuning on site using your actual mix and target block format
- Operator training covering hydraulic pressure adjustment within the 16–21 MPa range
- Mould change procedure demonstrated with the specific formats included in your order
- Scheduled inspection of vibration platform bearings and hydraulic seals during first-year warranty
What We Need to Quote Accurately
To size a fully automatic hollow brick production line correctly, share the exact block dimensions your market demands, the source and type of your local aggregate, and the daily output you need per format. Tell us the voltage and frequency at your site, the language your operators read on a screen, and the pallet size that fits your existing curing racks. If you already run upstream mixers or downstream stackers, include their throughput so the QT4-20 block machine specifications align with the rest of the line.
Frequently Asked Questions
Q: How is daily output calculated, and which block format does each figure assume?
A: Each output figure is tied to a specific block size, mould cavity count, and cycle time range. For example, 7,200–9,600 hollow bricks per day assumes a 400×200×200 mm format with 4 cavities and a 15–20 second cycle. We provide a full capacity table showing the format behind every number so you can plan against your actual product mix.
Q: How do I match vibration force and hydraulic pressure to my local aggregate?
A: Send us a representative sample of your crushed stone or sand, and we run test cycles at different pressure and vibration settings. The 16–21 MPa hydraulic range and 40 kN vibration force are adjusted based on results, then locked into the PLC recipe for consistent block density across production runs.
Q: Can the pallet size be changed to fit my existing curing racks and forklift?
A: The standard 1020×570 mm pallet can be swapped for alternative dimensions if your curing racks or forklift require it. We confirm the new pallet size against the moulding area and demolding stroke before finalising the machine design to avoid downstream handling conflicts.
Q: Which voltage, frequency, and PLC language options are available before shipment?
A: Voltage and frequency are configured to match your site supply, and the PLC display language is set to your operators’ preference. Both are confirmed in a written specification sheet before the QT4-20 enters production, preventing reprogramming delays during on-site commissioning.
Q: What documentation comes with the machine to support customs clearance and installation?
A: You receive a CE declaration where applicable, factory test records, hydraulic and electrical schematics, an operation manual in your chosen language, packing photographs, and a wear parts list with reorder numbers. Customs documentation support is included for the destination country’s import requirements.