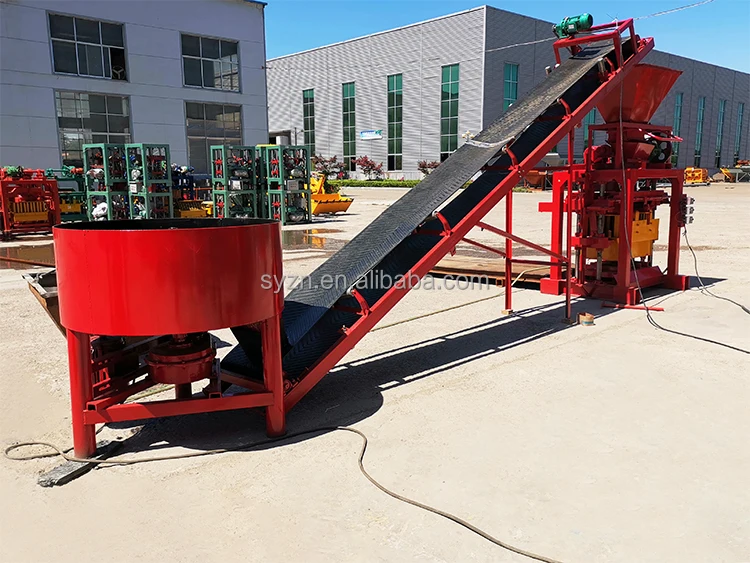
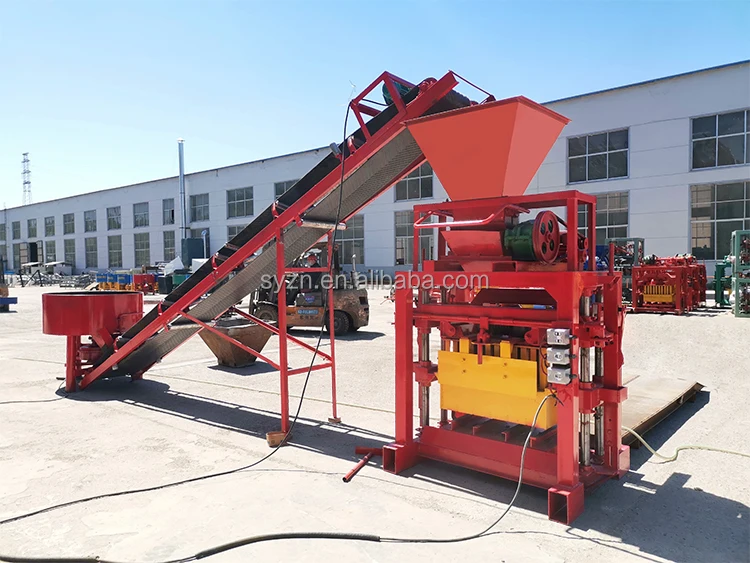
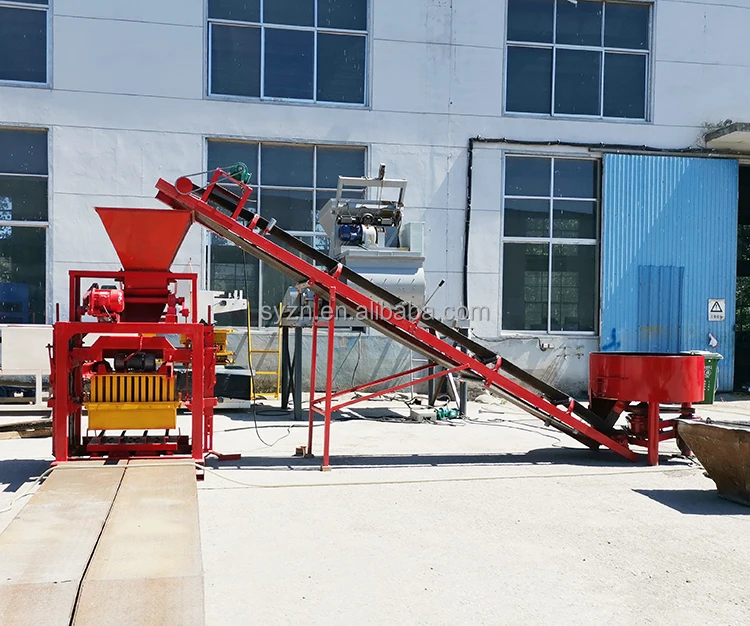
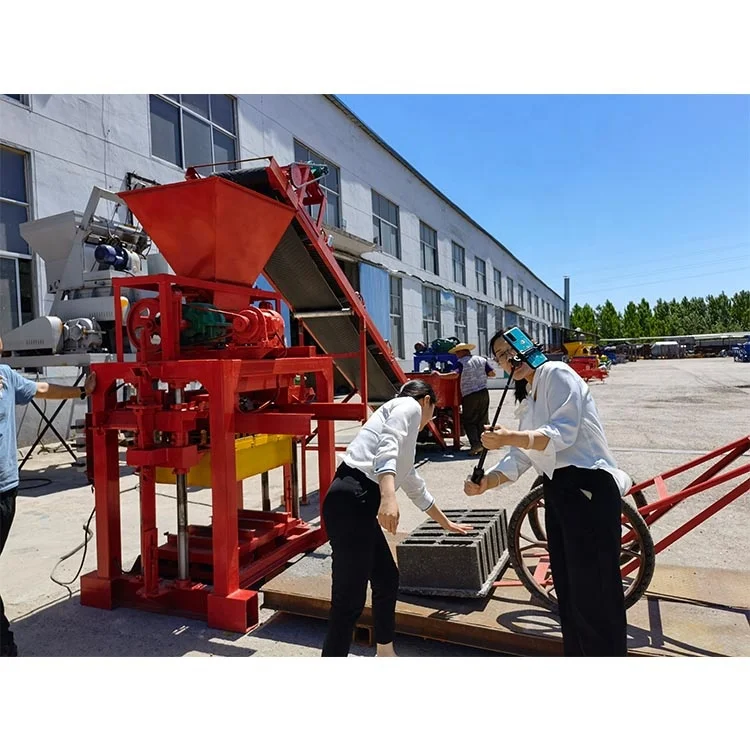
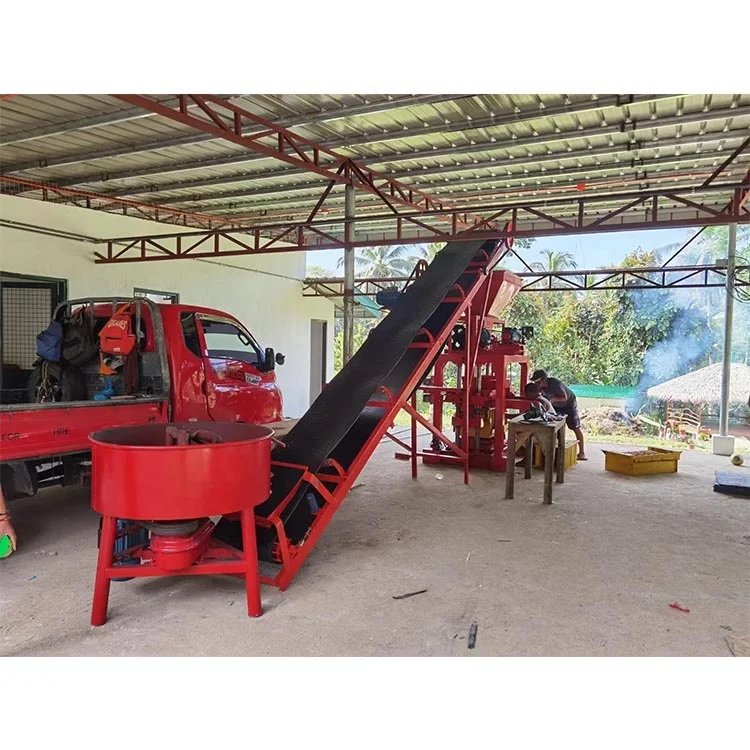
Description
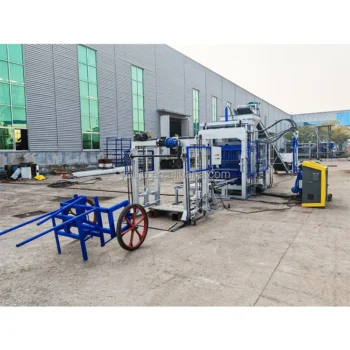
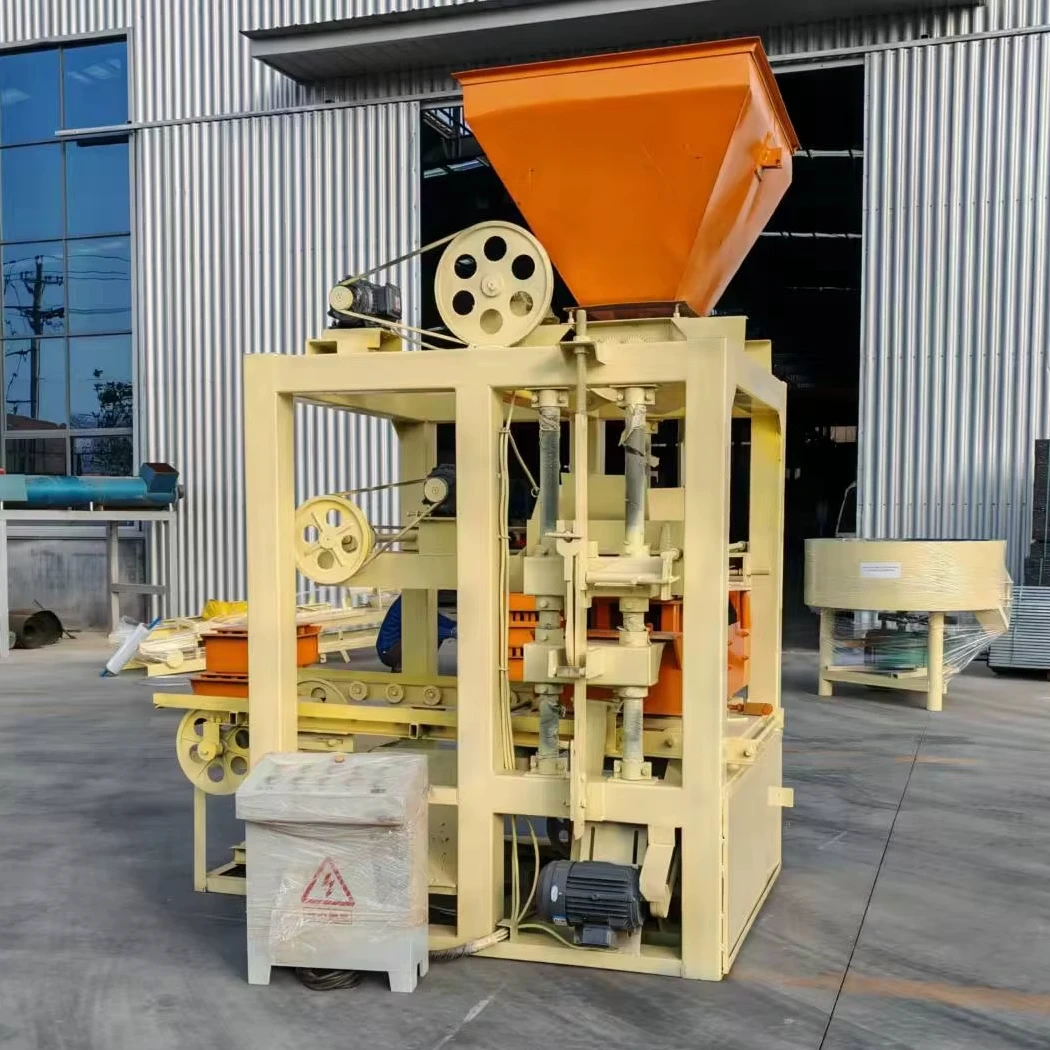
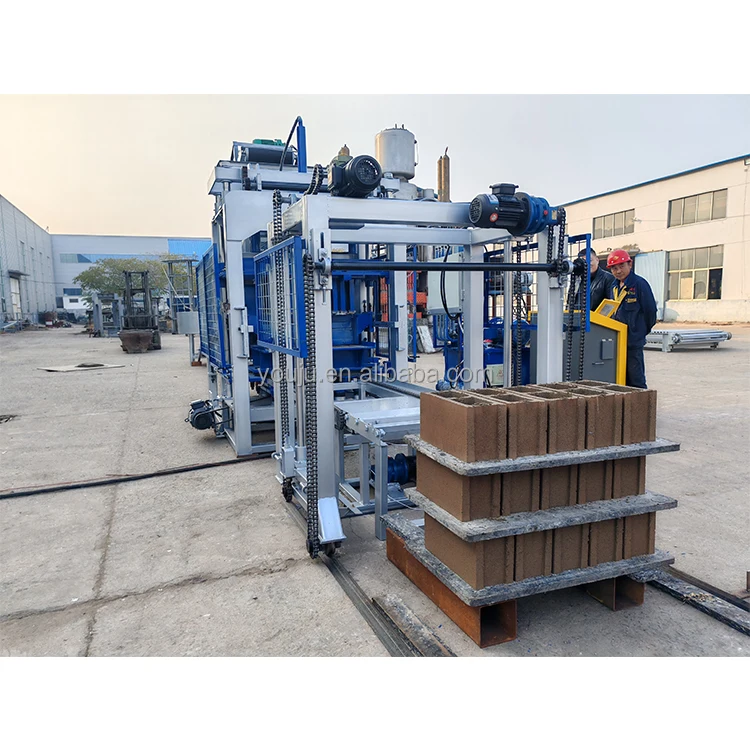
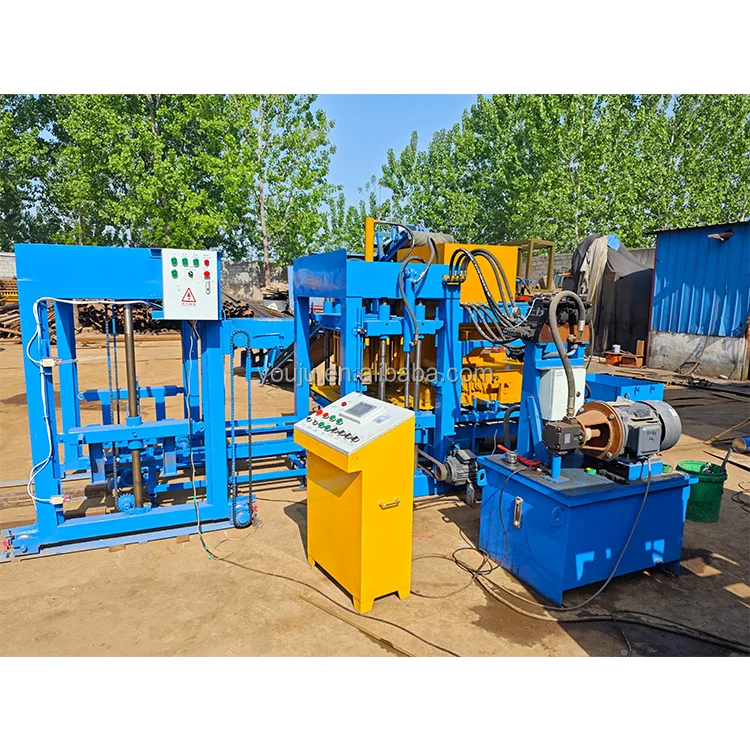
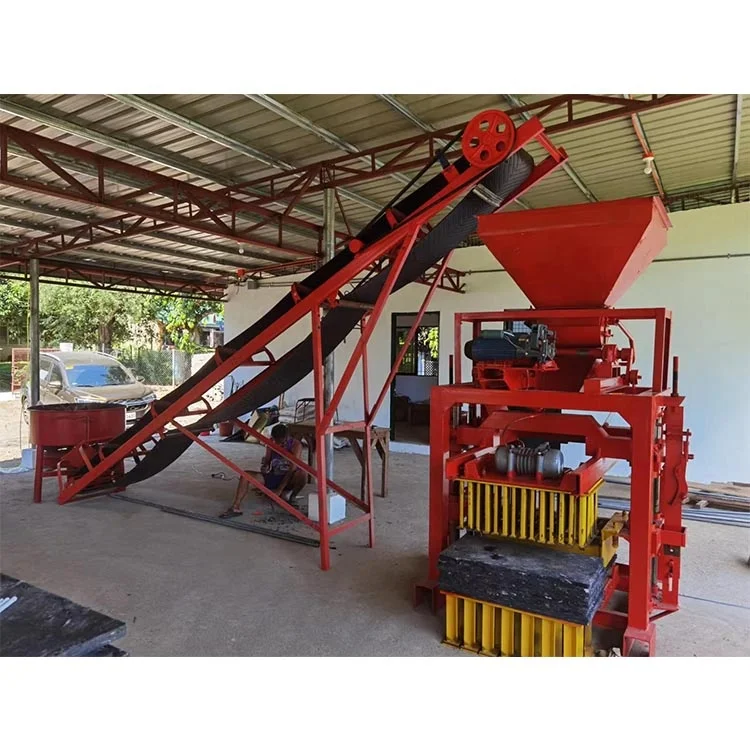
Matched system approach — machine, mould, pallet and handling specified as one cohesive unit rather than assembled from separate suppliers, ensuring the QTJ4-35 block machine specifications align with your actual production targets.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-35 |
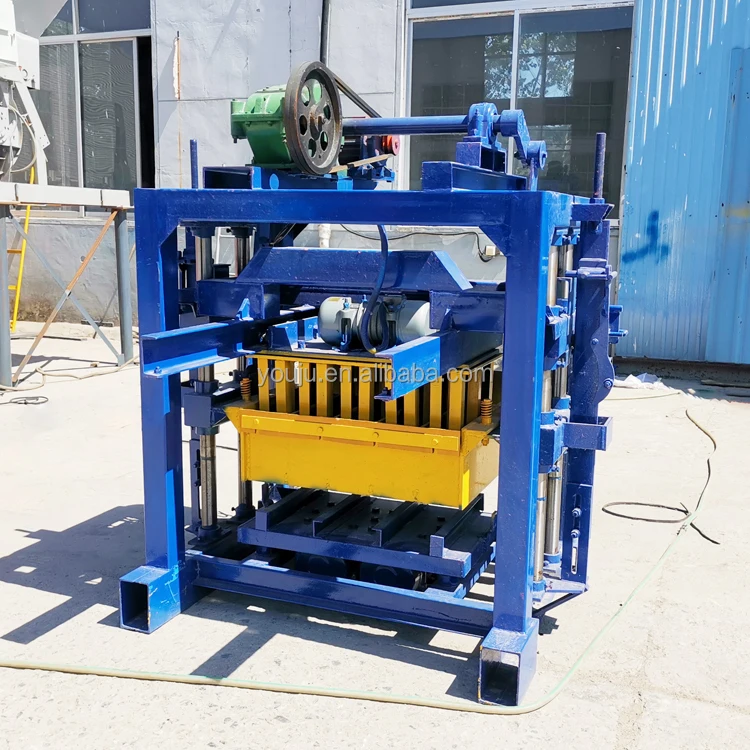
| Product Type | Stationary Block Making Machine |
| Overall Dimensions (L×W×H) | 2050×1660×1900 mm |
| Rated Exiting Force | 35 kN |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 2800 r/min |
| Pallet Size | 850×450 mm |
| Molding Cycle | 35 s (basis to be confirmed per block format) |
| Overall Power | 9.7 kW |
| Total Mass | 1500 kg |
| Demolding Method | Vibration |
| Factory Area | 260 m² |
| Raw Material | Crushed stone, sand, cement, dust, fly ash, gravel, slag |
| Automation Level | Manual / semi-automatic (manual pallet handling implied) |
| Hydraulic Pressure | N/A (vibration-based machine) |
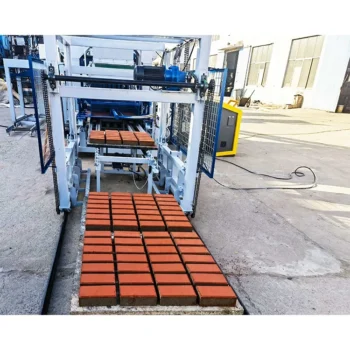
| Applied Products | Concrete blocks, hollow/solid blocks, pavers, interlocking blocks, curbstone |
| Warranty | 1 year (excluding spare parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Small-scale block production | Hollow and solid concrete blocks from crushed stone and cement |
| On-site construction projects | Standard building blocks using locally sourced sand and gravel |
| Paver and interlocking brick manufacturing | Colored pavers and interlocking formats with fine aggregate mixes |
| First-time block plant setup | Entry-level production using fly ash, slag, or stone dust blends |
What the "35-Second Cycle" Actually Means for Your Output
A molding cycle time only becomes meaningful when matched to the specific block format and thickness you intend to produce.
Many buyers receive quotations stating a cycle time without clarifying which product format that figure assumes. When you switch from a standard hollow block to a thinner paving format, the actual cycle may differ, and your daily output falls short of the original expectation. The QTJ4-35 block machine specifications list a 35-second cycle, but verifying this against your target block dimensions prevents planning errors [NEED_CITE: block machine cycle time assumptions by format].
Platform Vibration and Aggregate Matching
The platform vibration system operates at 2800 r/min with a rated exiting force of 35 kN. This vibration profile must align with your local aggregate characteristics and mix design. I once saw a situation where a machine configured for standard river sand was shipped to a site using volcanic ash aggregate — the vibration force and feeding time were completely mismatched, resulting in blocks that crumbled under hand pressure. Before finalizing any QTJ4-35 block machine specifications, confirming your exact raw material blend ensures the vibration parameters are set correctly from the start.
Pallet Size and Your Existing Curing Setup
The 850×450 mm pallet dimension dictates how many blocks cure per rack and whether your existing forklift can handle the loaded pallets efficiently. If your curing area was designed around a different pallet standard, you face either wasted floor space or the cost of replacing your material handling equipment. Checking pallet compatibility against your current infrastructure avoids unexpected capital expenditure after the machine arrives [NEED_CITE: pallet handling standards in block production].
Understanding Vibration Force and Compaction Density
On a vibration-based stationary block machine like this, the rated exiting force and vibration frequency work together to compact the concrete mix into the mould cavity. Higher frequency with lower force suits finer aggregates and thinner products, while heavier mixes with larger aggregate require sustained force to achieve adequate density. The 35 kN rating on the QTJ4-35 positions it for small to medium-format blocks using standard concrete mixes. Understanding this relationship helps you evaluate whether the machine matches your target block strength requirements without over- or under-specifying the equipment.
The Cost of Skipping Mix Design Verification
When the vibration parameters are set for a generic mix rather than your actual raw materials, the consequences compound quickly. Blocks may pass visual inspection but fail compressive strength tests, leading to rejected batches and reputation damage with your customers. The time spent recalibrating after arrival — plus the material waste during trial runs — often exceeds what a pre-shipment mix verification would have cost [NEED_CITE: concrete block compressive strength testing standards].
Why Sourcing From a Single-Focus Supplier Matters
Block machinery as a dedicated focus means the machine, mould, pallet and handling equipment are specified as an integrated system rather than pieced together from unrelated vendors. Configuration decisions are made against your actual mix design and target format, not a catalogue default. Mould design covers the formats your market actually sells, with custom drawings available. The automation level allows you to start with manual pallet handling and plan for future upgrades. Installation includes operator training so your team understands mould change procedures and maintenance intervals from day one.
Documentation & Verification
- Line layout showing the 260 m² factory area allocation with curing rack positions
- Capacity calculation stating which block format the 35-second cycle assumes
- Mould drawing and format list confirming interchangeable options before order
- Pallet material and dimension specification matched to your forklift capacity
- Voltage and frequency confirmation document prior to production start
- Factory test record using your specified raw material blend where possible
Installation, Commissioning & Support
- Foundation preparation for the 2050×1660 mm footprint with level tolerance requirements
- Dedicated power circuit for the 9.7 kW total load with correct voltage and frequency
- Machine arrives fully assembled, requiring only utility connections and pallet loading
- Vibration frequency and molding cycle parameter setting during initial commissioning
- Operator training covering mould change procedure and platform vibration maintenance
- Wear parts list identifying vibration motor brushes and mould liner replacement intervals
Preparing Your Inquiry With the Right Details
To receive an accurate configuration rather than a generic quotation, share your target block format with dimensions, your daily output requirement, and the raw materials available locally. Include your site voltage and frequency, plus any existing pallet or forklift specifications you need the system to match. This information allows the proposal to address your actual production scenario.
Frequently Asked Questions
Q: How is daily output calculated for the QTJ4-35 — which block format is assumed?
A: The 35-second molding cycle must be verified against your specific block format and thickness. A standard hollow block and a thin paver have different compaction and demolding requirements. Request a capacity calculation that names the exact product dimension used for the output projection, so you can plan shifts and curing space accurately.
Q: Is the vibration force matched to my local aggregate and mix design?
A: The 2800 r/min frequency and 35 kN exiting force suit standard concrete mixes with common aggregates. If your region uses volcanic ash, lightweight aggregate, or high fly-ash content blends, the vibration parameters may need adjustment. Providing your mix design before order allows verification that the platform vibration achieves target block density.
Q: How long does a mould change take, and what tools are needed?
A: Mould interchangeability is a feature of this machine class, but changeover time depends on the format difference and operator familiarity. Confirming the procedure and required tools before purchase ensures your team can switch formats within a practical window rather than losing most of a shift to the changeover.
Q: What pallet size and material should I choose for my curing area?
A: The standard 850×450 mm pallet must align with your curing rack spacing and forklift capacity. Bamboo, hardwood, and composite pallets each have different weight and durability characteristics. Matching pallet specification to your existing handling infrastructure prevents bottlenecks between the press and the curing zone [NEED_CITE: pallet material selection for concrete block curing].