Description
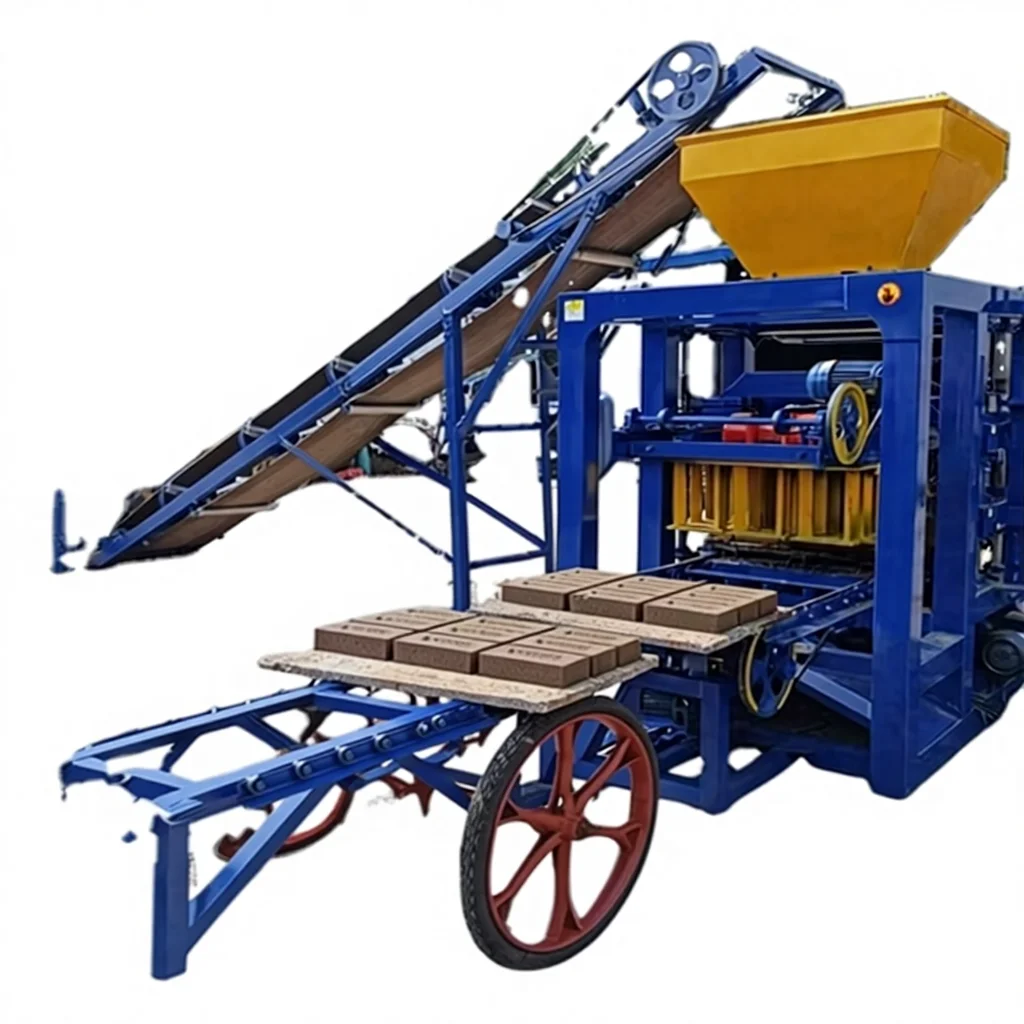
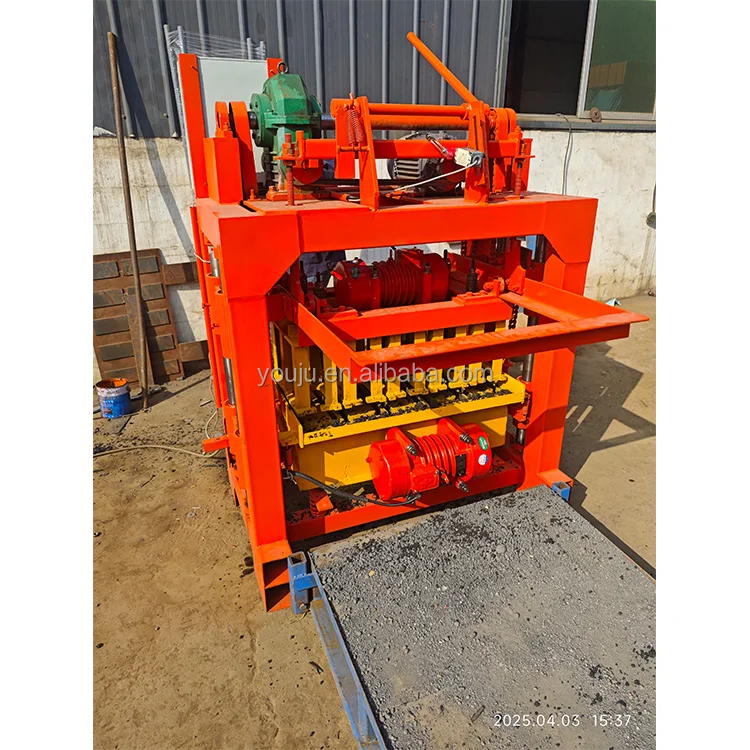
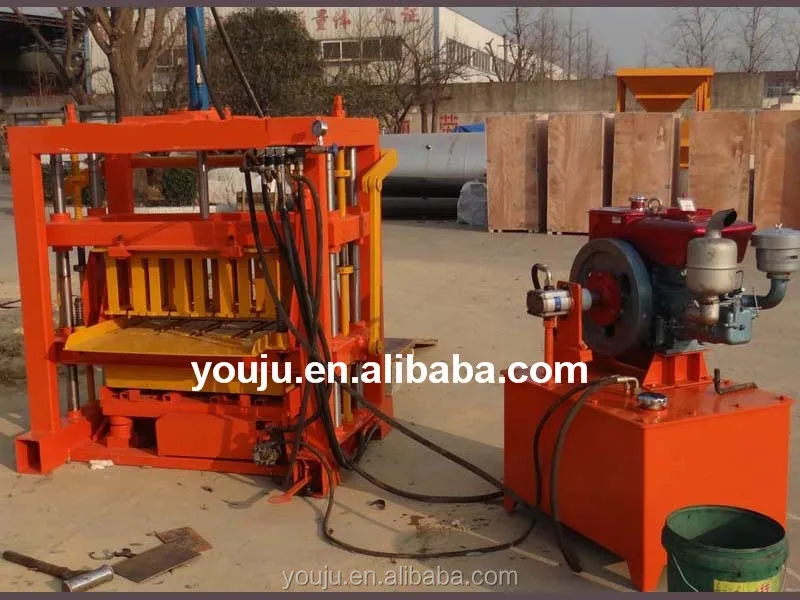
Matched system — the QTJ4-40 block making machine, moulds and pallets are specified together against your actual mix design and target format, not pulled from separate catalogues.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-40 |
| Product Type | Manual Concrete Block Making Machine |
| Rated Power | 9.5 kW |
| Voltage & Frequency | Configurable to buyer local supply (basis to be confirmed) |
| Control System | Manual operation |
| Overall Dimensions (L×W×H) | 1350 × 1460 × 1800 mm |
| Net Weight | 1000 kg |
| Vibration Frequency | 2800 r/min |
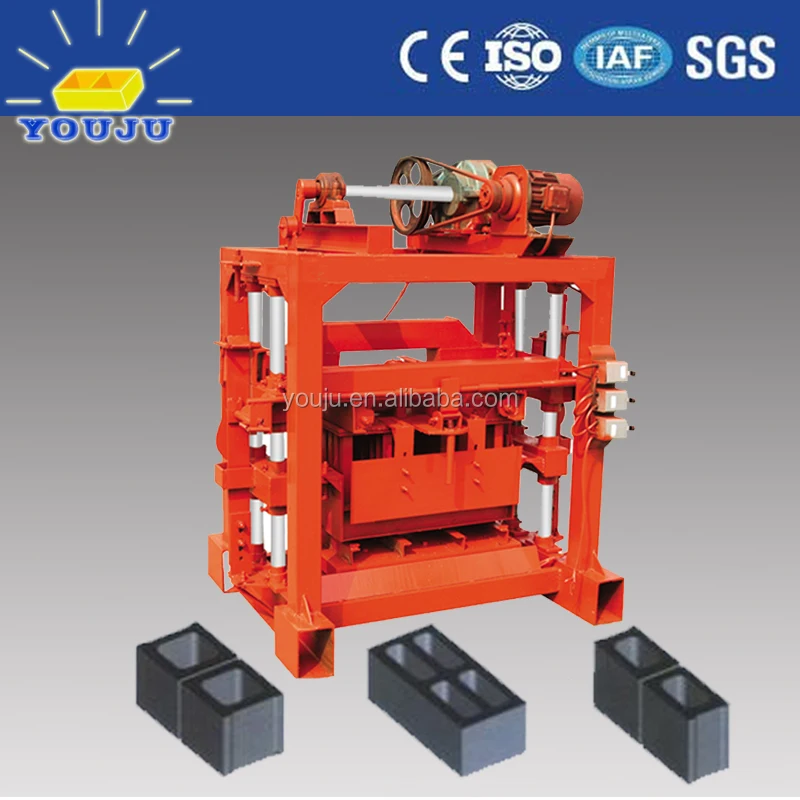
| Standard Mould Format | 390 × 190 × 190 mm / 4 pcs per mould |
| Output per Cycle | 4 pcs (basis to be confirmed) |
| Workers Required | 3–5 |
| Mould Change | Interchangeable moulds, custom design available |
| Warranty | 1 year |
Application Suitability
| Application | Material or Output |
|---|---|
| Small-scale hollow block plants | Cement, crushed stone, sand and water mix for 390×190×190 mm hollow blocks |
| On-site contractor production | Local aggregate and cement for solid and hollow blocks at project locations |
| First-time block entrepreneurs | Standard hollow and solid formats using regionally sourced raw materials |
| Distributors adding basic formats | Interchangeable moulds for multiple block types on a single press |
What "4 Pieces per Cycle" Actually Means for Your Daily Plan
Cycle count alone does not tell you how many saleable blocks you will produce in a shift.
When I first started handling orders for the QTJ4-40 block making machine, buyers would see "4 pcs per mould" and multiply it by cycles per hour to project daily revenue. That calculation ignores the time spent on manual pallet handling, feeding raw material into the hopper, moving cured blocks off the pallets, and cleaning the mould between runs. One buyer in West Africa assumed a continuous cycle pace and planned his delivery schedule around a figure the press could never sustain once operator fatigue and material batching delays were factored in. The real daily output depends on how your workers move pallets, how fast your mixer feeds the hopper, and how your local aggregate behaves under vibration [NEED_CITE: factors affecting manual block press throughput].
Mould Format and the Blocks Your Market Actually Buys
The standard mould produces four 390 × 190 × 190 mm hollow blocks per cycle. If your local construction market demands a different dimension — solid blocks, interlocking pavers, or a non-standard hollow format — the QTJ4-40 block making machine accepts interchangeable moulds, and custom moulds can be built to your drawings. Confirming the exact block format before production starts means the machine arrives ready to press the product your customers order, not a catalogue default that sits idle.
Vibration, Pressure and Local Aggregate Behaviour
Block strength comes from how well the vibration force compacts your specific mix. The 2800 r/min vibration frequency on this press is paired with a high-force vibration motor, but the resulting density depends on your aggregate gradation, cement ratio and moisture content. A mix that works in a dry climate with clean washed sand will behave differently under the same vibration settings as a mix using locally available laterite or unwashed crusher dust. We set the vibration parameters against your material sample so the blocks leaving the press meet the compressive strength your market requires [NEED_CITE: vibration compaction and aggregate gradation in block making].
Power, Voltage and the Commissioning Delay You Can Avoid
The 9.5 kW rated power must be matched to your site’s voltage and frequency before the machine enters production. I have seen machines sit in containers at the port because the buyer’s local supply was 220V/60Hz while the motor was wound for 380V/50Hz — a mismatch that could have been resolved with a single confirmation email. The QTJ4-40 specifications include voltage configuration to your local supply, and we document the exact voltage, frequency and any control language requirements before fabrication begins.
Reading the Specs That Matter for Daily Production
The vibration frequency of 2800 r/min determines how rapidly the mix particles settle into the mould cavity — higher frequency generally produces a denser block face and more consistent wall thickness in hollow formats. The 1000 kg net weight provides the mass needed to absorb vibration recoil, keeping the frame stable across thousands of cycles without bolt loosening. Overall dimensions of 1350 × 1460 × 1800 mm define the floor space the press occupies, but you must also allow room for pallet staging on the feed side and cleared block removal on the output side. The 3–5 worker requirement reflects manual pallet handling; if you plan to add a pallet feeder or stacking system later, the press footprint and cycle rhythm must accommodate those stations without creating a bottleneck.
The Cost of Skipping Format and Material Confirmation
Ordering a block press without confirming your target format and mix design leads to problems that surface only after installation. Moulds that do not match local building codes force a second purchase and weeks of downtime. A machine configured for clean silica sand struggles to compact the clay-heavy aggregate available at your site, producing blocks that crumble at the edges and fail compressive strength tests. Voltage mismatches delay commissioning while a replacement motor is sourced locally at a premium [NEED_CITE: common causes of block machine commissioning delays]. These are not hypothetical — they are the phone calls I receive from buyers who ordered from a catalogue without a single question about their material.
Why Buyers Source This Machine Here
Block machinery is our single focus, which means the QTJ4-40 press, its moulds, pallets and handling equipment are specified as one matched system. Configuration is set against your actual mix design and local aggregate, not a factory default that assumes material you cannot source. Mould design covers the formats your market sells, including custom drawings for non-standard dimensions. The automation level is selectable — you can start with manual pallet handling on the QTJ4-40 and plan an upgrade path as volume grows. Installation and commissioning support includes operator training so your team knows mould change procedures, vibration adjustment and daily maintenance from the first shift.
Documentation & Verification
- Line layout showing QTJ4-40 placement with pallet staging and curing area flow
- Capacity calculation stating the exact block format used for output projection
- Mould drawing and format list confirming dimensions before fabrication
- Voltage and frequency confirmation sheet signed off before production starts
- Factory test record on your specified mix and mould format before dispatch
Installation, Commissioning & Support
- Foundation pad sized to the 1350 × 1460 mm footprint with vibration isolation
- Dedicated 9.5 kW circuit matching your confirmed voltage and frequency
- Machine shipped assembled with mould installed for rapid first-day startup
- On-site vibration frequency and feed timing adjusted to your local aggregate
- Operator training covering mould change, pallet handling and daily greasing points
- Wear parts list supplied so replacement springs and liner plates are on hand
What to Include in Your Inquiry
Send us the block format your market buys most, the daily volume you need to hit, and a description of your local aggregate including source and gradation. Include your site voltage, frequency and the language your operators read so the control markings match. If you already have a mixer, pallets or curing racks, tell us the specifications so the QTJ4-40 block making machine is configured to fit your existing line rather than arriving as an isolated press.
Frequently Asked Questions
Q: How is daily output calculated for the QTJ4-40, and which block format is that figure based on?
A: Daily output depends on the block format, your cycle rhythm including manual pallet handling time, mixer feed rate and worker pace. We calculate capacity based on the specific mould format you confirm — typically 390 × 190 × 190 mm hollow blocks — and state the assumed cycle time so your production plan matches reality rather than a theoretical maximum.
Q: Which mould formats are available, and how long does a mould change take?
A: The standard mould produces 390 × 190 × 190 mm hollow blocks, and custom moulds can be built to your drawings for solid blocks, pavers or other formats. Mould change involves unbolting the current mould, lifting it clear and securing the replacement — a process your operators learn during commissioning training so format switches do not consume an entire shift.
Q: How do you confirm voltage, frequency and control display language before shipment?
A: We send a voltage and control confirmation sheet listing your exact supply specifications and operator language preference. You sign off before production begins, so the motor winding and any control labels match your site conditions on arrival, avoiding the commissioning delays that unconfirmed electrical specs cause.
Q: Can the machine be configured for my local aggregate rather than a default setting?
A: Yes. We ask for a description of your aggregate — source, gradation, moisture behaviour — and set vibration parameters accordingly. A mix using unwashed crusher dust compacts differently under the 2800 r/min vibration than clean washed sand, and the press is adjusted to produce consistent block density with your actual material.
Q: What supporting equipment should be matched to the QTJ4-40 so cycle time is not lost?
A: A pan mixer sized to fill the hopper between cycles, manual or semi-automatic pallet feeding, and a curing area with pallets matching the press output keep the machine running. We specify these stations together so the press is not left idle waiting for material, pallets or cleared space downstream.