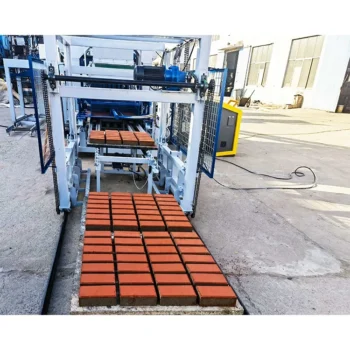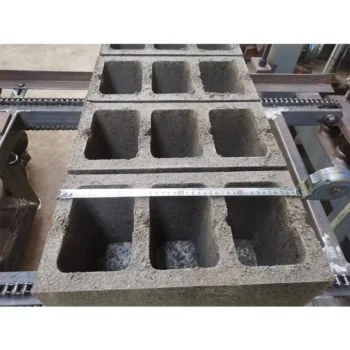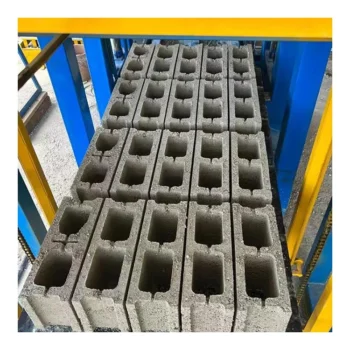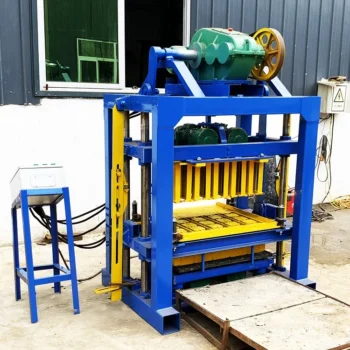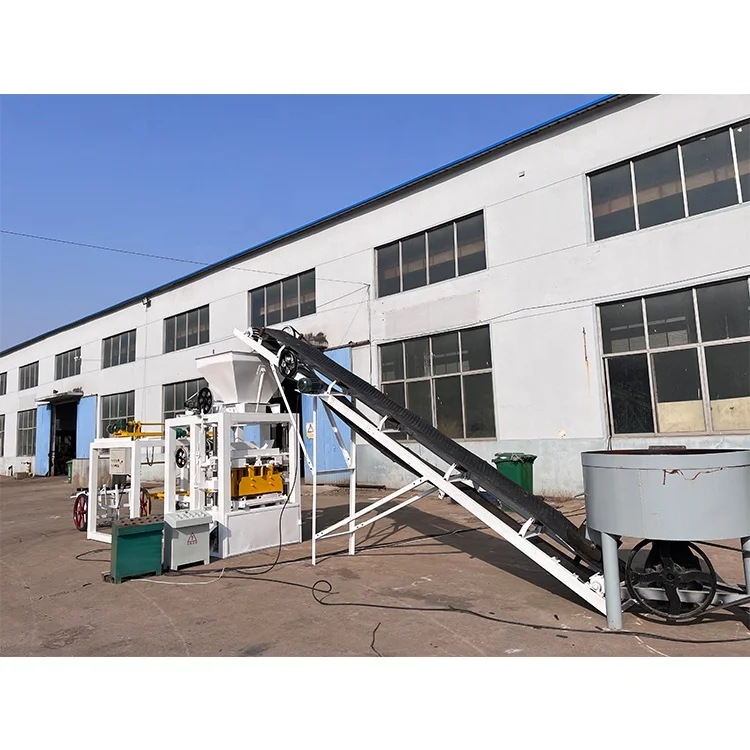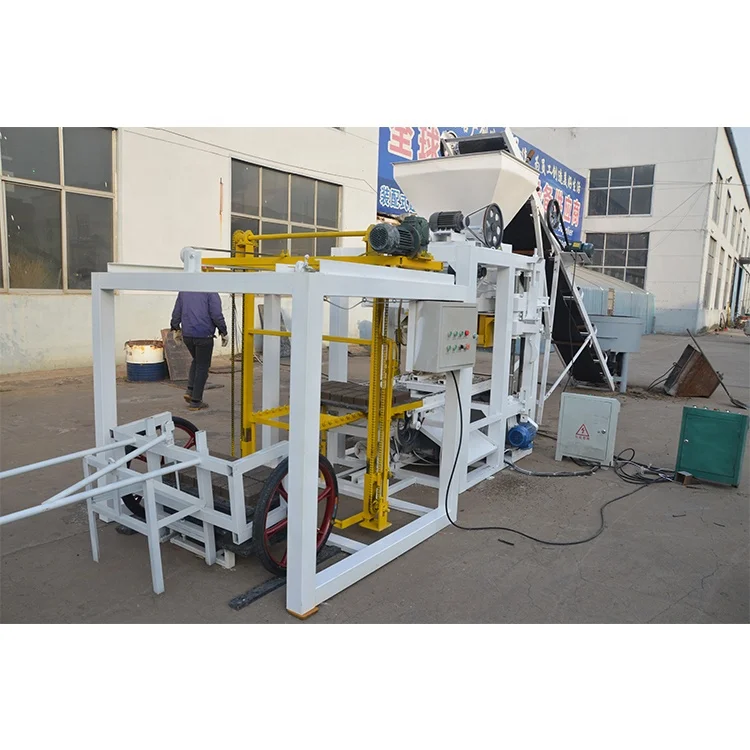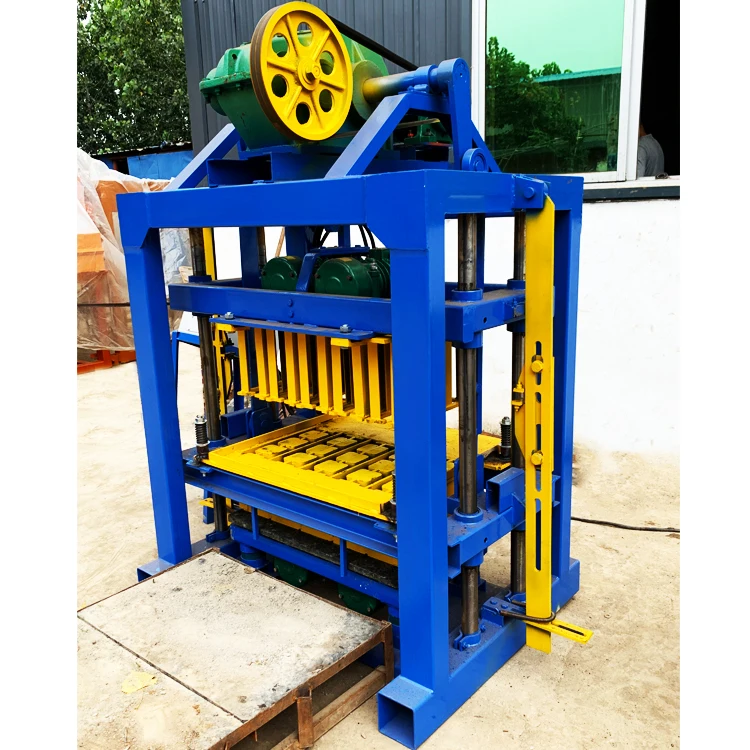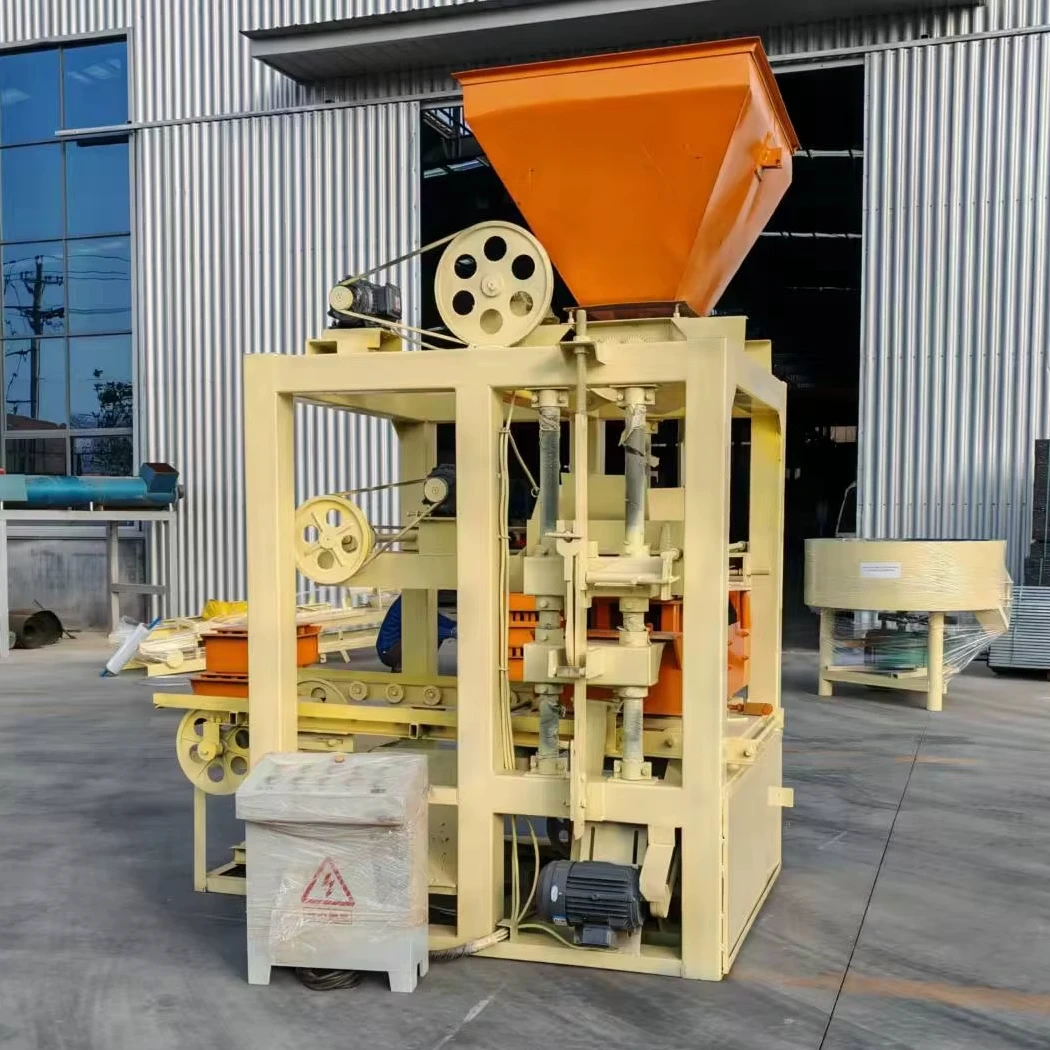
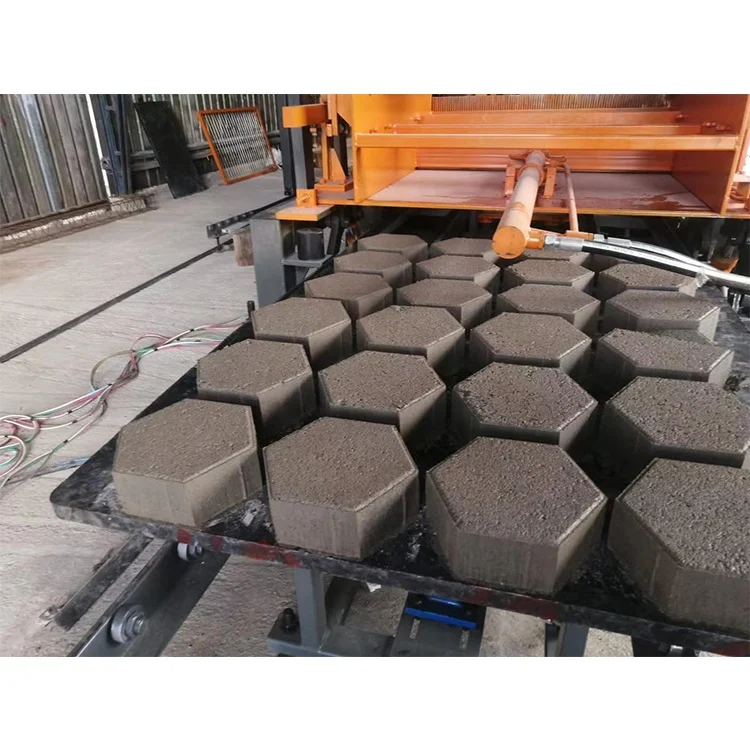
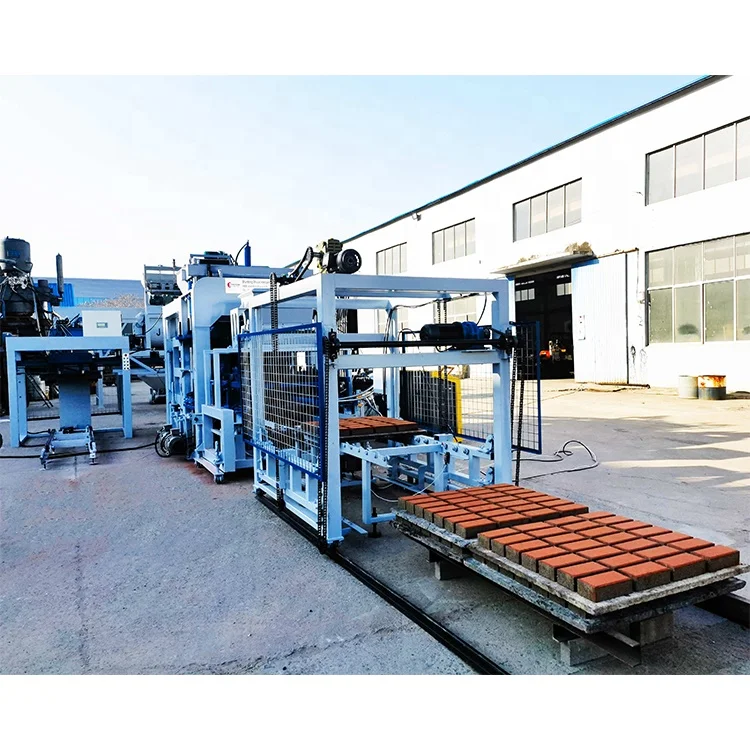
Description
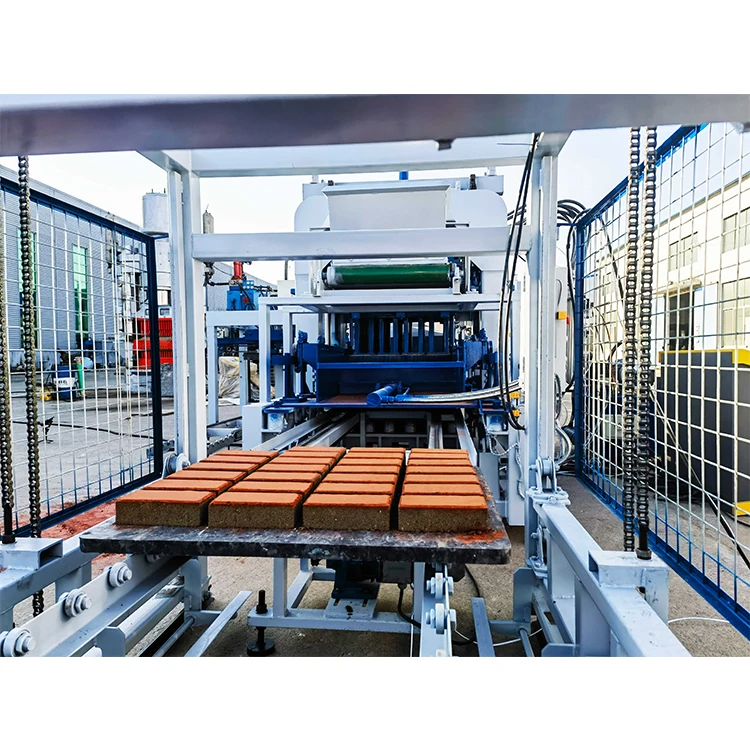
Mould-to-press matching — cycle time, pallet footprint and vibration profile are locked to your paver format before the line ships, not guessed from a catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT8-15 |
| Product Type | Concrete Paver Block Making Machine |
| Overall Dimension | 8300 × 1860 × 3000 mm |
| Total Mass | 9 T |
| Rated Pressure | 21 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 2800–4500 r/min |
| Vibration Force | 60 KN |
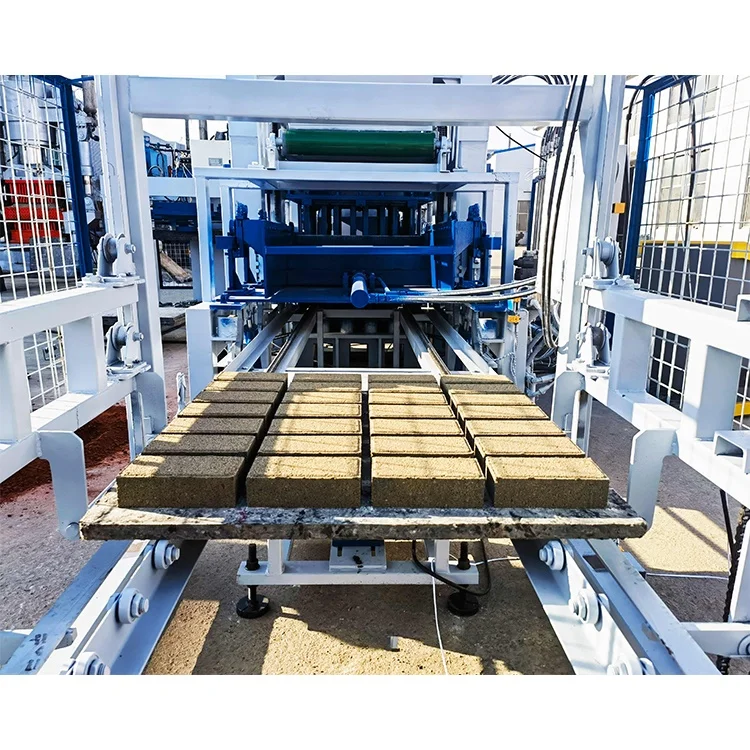
| Pallet Size | 950 × 900 mm |
| Molding Cycle | 15–25 s (basis not stated in source) |
| Overall Power | 55.5 kW |
| Demolding Method | Hydraulic |
| General Water Consumption | 12 T/Day |
| Factory Area | 600 m² |
| Control System | PLC aptitude control with human-machine interface dialogue |
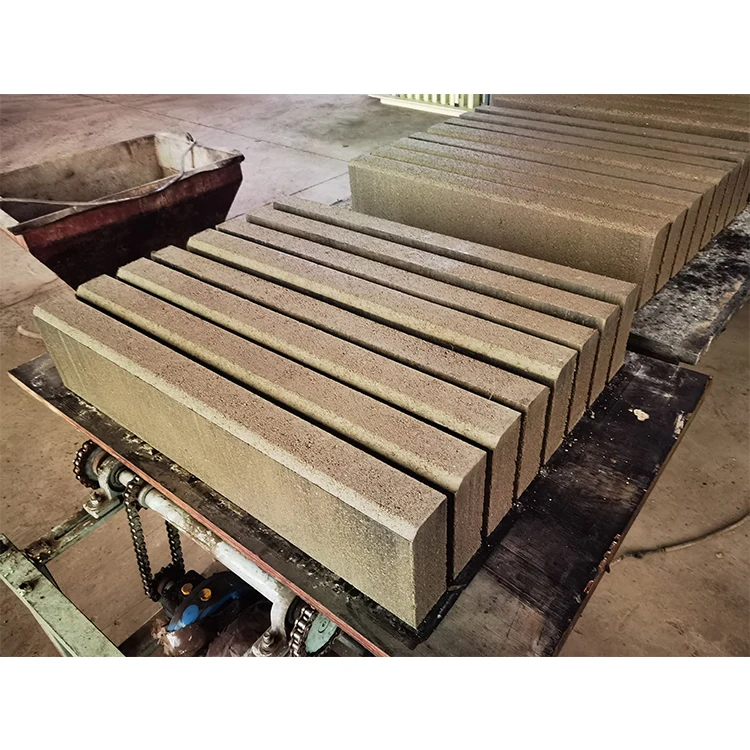
| Applied Products | Concrete blocks, hollow/solid blocks, pavers, interlocking blocks, curbstone, colored pavers |
| Raw Material | Crushed stone, sand, cement, dust, fly ash, gravel, slag |
Application Suitability
| Application | Material or Output |
|---|---|
| Interlocking paver production for municipal walkways | Crushed stone and cement blends with pigment dosing |
| Colored paver runs for residential driveways | Sand, cement and oxide pigment on 950 × 900 mm pallets |
| Curbstone forming for road edge profiles | Coarse aggregate and cement at higher hydraulic pressure |
| Hollow block output for partition walls | Fly ash or slag mixed with sand and cement |
| Solid block runs for load-bearing walls | Gravel and cement with extended vibration dwell |
What "15-25 Seconds per Cycle" Actually Means for Your Paver Line
Cycle time is a range, not a promise — the block format, mix moisture and pallet condition decide where you land inside it.
When a supplier quotes a Concrete Paver Block Making Machine specifications sheet listing 15-25 seconds, that span covers everything from a thin 60 mm paver on a dry mix to an 80 mm interlocking block with high fly-ash content. I have watched buyers sign off on a cycle figure, then discover on commissioning day that their local sand holds more moisture than the test mix, stretching every cycle toward the upper end and cutting daily output by a noticeable margin [NEED_CITE: effect of aggregate moisture on concrete block cycle time]. The honest move is to confirm which format and which mix produced the quoted number, then re-calculate against your own raw material.
Pallet Footprint and Curing Area Alignment
The 950 × 900 mm pallet governs how many pavers you press per cycle, but it also dictates the lane width in your curing racks and the fork tine spacing on your existing lift trucks. If the pallet size is chosen without checking the curing yard, wet blocks end up stacked on the floor because the racks were built for a smaller footprint. Every Concrete Paver Block Making Machine specifications review should start with the buyer’s current handling gear, then work backward to the press.
Vibration Force Meets Hydraulic Pressure
Sixty kilonewtons of platform vibration combined with 21 MPa hydraulic pressure determines how densely the mix is compacted inside the mould cavity. A porous paver needs lower compaction so water passes through; a heavy-duty driveway paver needs the full force to reach the compressive strength the project specifies. Tuning vibration frequency between 2800 and 4500 r/min lets the operator shift between formats without swapping mechanical parts, keeping the Concrete Paver Block Making Machine flexible across product runs [NEED_CITE: vibration frequency adjustment for different concrete block densities].
Reading the Specs That Matter Most
Overall power of 55.5 kW tells you the electrical service must carry sustained motor load plus vibration motor peaks — undersizing the transformer causes PLC resets mid-cycle. The 15-25 second molding cycle is governed by block thickness as much as mix design; a 100 mm curbstone holds the mould longer than a 60 mm paver, so capacity calculations must state the format. Platform vibration at up to 4500 r/min transmits energy through the pallet into the mix, meaning pallet flatness and stiffness directly affect surface finish. The PLC human-machine interface lets the operator store recipes per format, reducing setup error when switching from interlocking pavers to hollow blocks within the same shift.
The Cost of Skipping the Mix Audit
Ordering a paver machine without testing your local aggregate locks you into a recipe the press was never tuned for. Vibration amplitude that works on river sand may leave wind-blown desert sand under-compacted, producing pavers that chip at the edges during demoulding. Buyers who skip this step often spend weeks adjusting parameters on site, losing saleable output while the machine sits idle [NEED_CITE: impact of ungraded local aggregate on concrete block strength]. A lab trial on your actual crushed stone and sand, run before the machine leaves the factory, removes most of that risk.
Why This Line Holds Up Across Formats
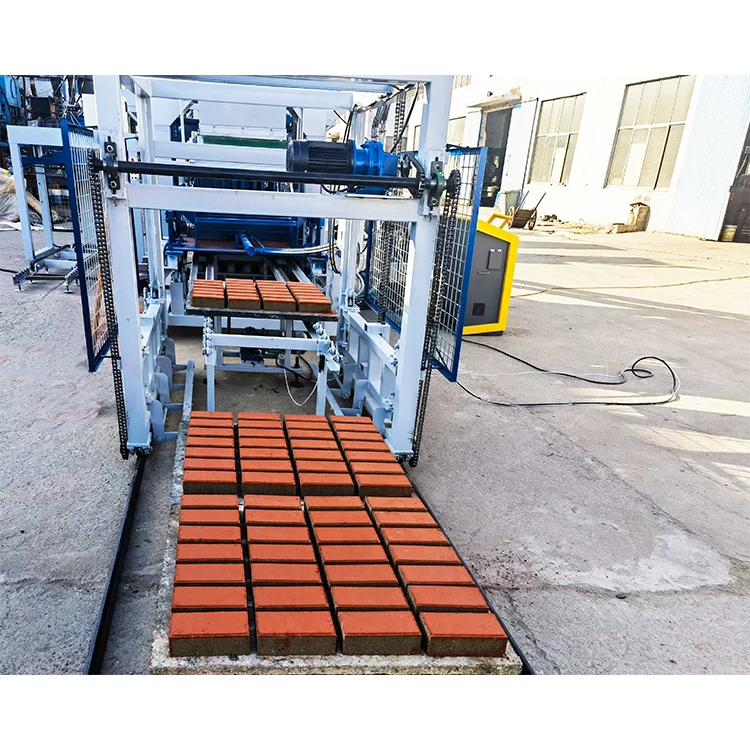
Block machinery is the only product category here, so press, mould, pallet and handling gear are specced as one system rather than sourced from separate vendors. Mould drawings are prepared against the paver shapes your market actually moves, not a generic sample book. Pallet size is confirmed against your curing racks and forklift before steel is cut. Voltage, frequency and PLC language are locked in before the crate closes, avoiding the silent delays that strand machines on docks. Factory test records cover your chosen block format, not a default setting the operator will never use.
Documentation & Verification
- Line layout showing pallet flow from press to curing rack with format-specific cycle times
- Mould drawing and format list confirming cavity count for each paver profile
- Pallet spec sheet matched to your existing fork truck and rack dimensions
- Voltage, frequency and PLC display language sign-off before crating
- Factory test record run on your target paver format and mix sample
- Hydraulic and electrical schematic with spare part cross-reference
Installation, Commissioning & Support
- 600 m² factory area requirement confirmed against your slab bearing capacity
- 55.5 kW total load checked with your local electrician for dedicated circuit sizing
- Platform vibration isolators leveled on site to prevent resonance transfer to curing racks
- PLC dialogue language set to operator preference before first production run
- Mould change procedure walked through with shift crew on your two main paver formats
- Wear part list cross-referenced to local bearing and seal suppliers for faster replenishment
What to Send With Your Inquiry
Share the paver profiles you plan to run, including thickness and whether interlocking lugs are required, so the mould cavities can be laid out on the 950 × 900 mm pallet. Confirm your local aggregate type, moisture range and whether fly ash is available, because these shift the vibration frequency window. Provide your site voltage and frequency, plus the language your operators read, so the PLC is configured before dispatch.
Frequently Asked Questions
Q: How is daily output calculated for each paver format on the QT8-15?
A: We start with the molding cycle for your specific paver thickness and mix, multiply by pallets per hour, then by cavities per mould on the 950 × 900 mm pallet. The result is stated per format, not blended across sizes, so you see realistic numbers for the products you actually sell.
Q: Which pallet size and material suits my curing area and forklift?
A: The standard 950 × 900 mm pallet must clear your curing rack lanes and match your fork truck tine spacing. We confirm rack width and lift capacity with you before finalizing pallet material — bamboo, PVC or steel — so wet blocks move from press to cure without manual re-stacking.
Q: How long does a mould change take between paver and hollow block formats?
A: Changeover depends on whether your line includes a quick-clamp mould frame. On a manual bolt-down setup, expect a portion of the shift; with hydraulic clamping, the swap shortens considerably. We time the procedure during factory acceptance using your two primary formats so you know the real figure.
Q: Can the machine be configured for my local aggregate and mix design?
A: Yes. Vibration frequency between 2800 and 4500 r/min and hydraulic pressure up to 21 MPa are adjusted after a trial on your actual sand, crushed stone or fly ash sample. The PLC stores the resulting recipe, letting operators recall it by format name on the human-machine interface.
Q: What block strength can I expect with my raw materials?
A: Strength depends on aggregate grading, cement ratio and compaction achieved at your chosen vibration setting. We run a sample batch on your material during factory testing and record demoulding strength and 28-day projection, giving you a baseline before the machine ships.