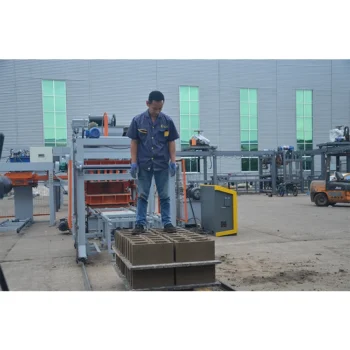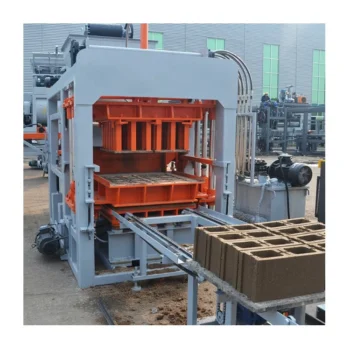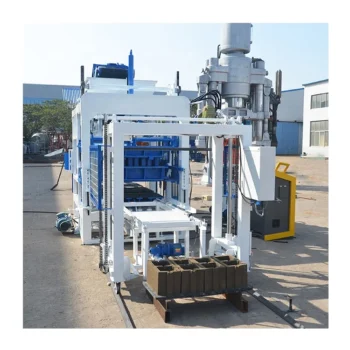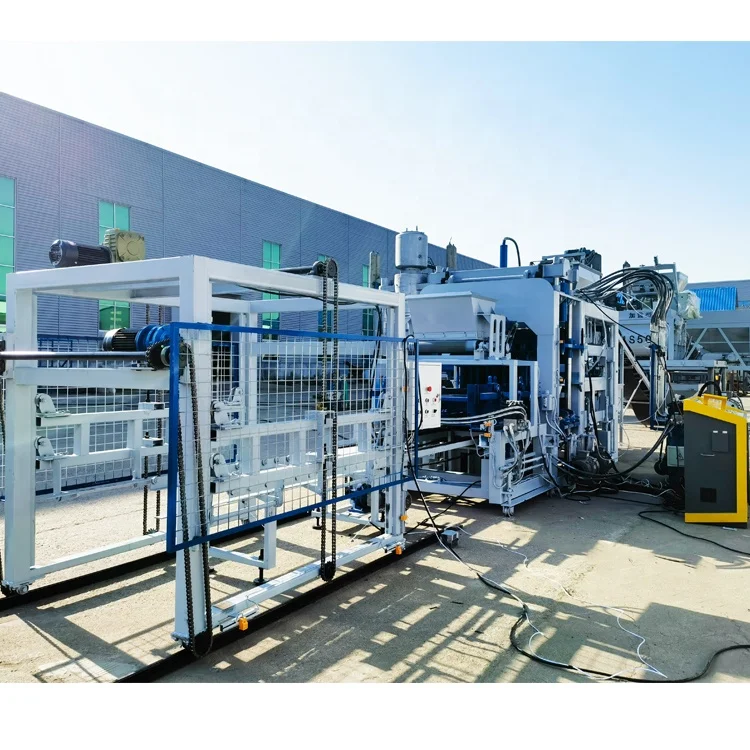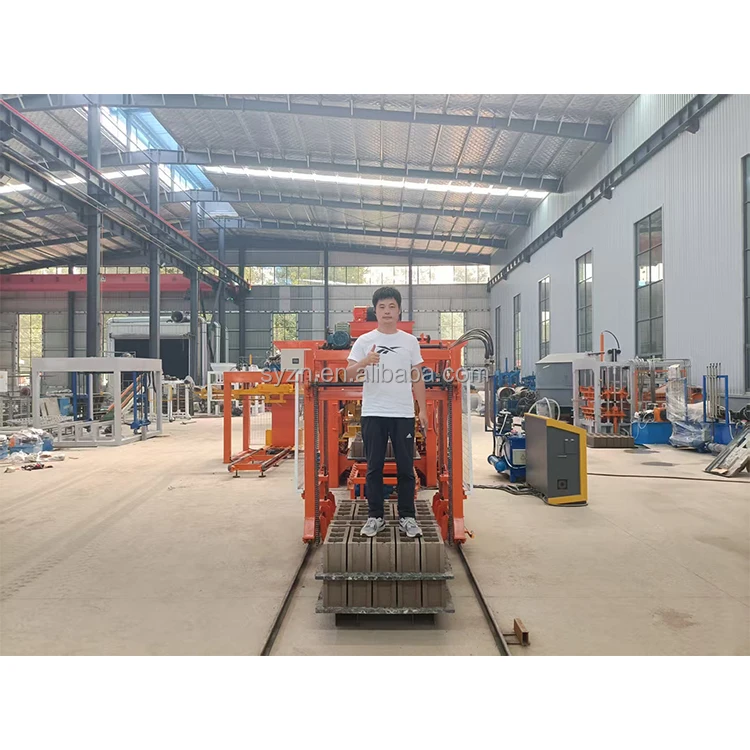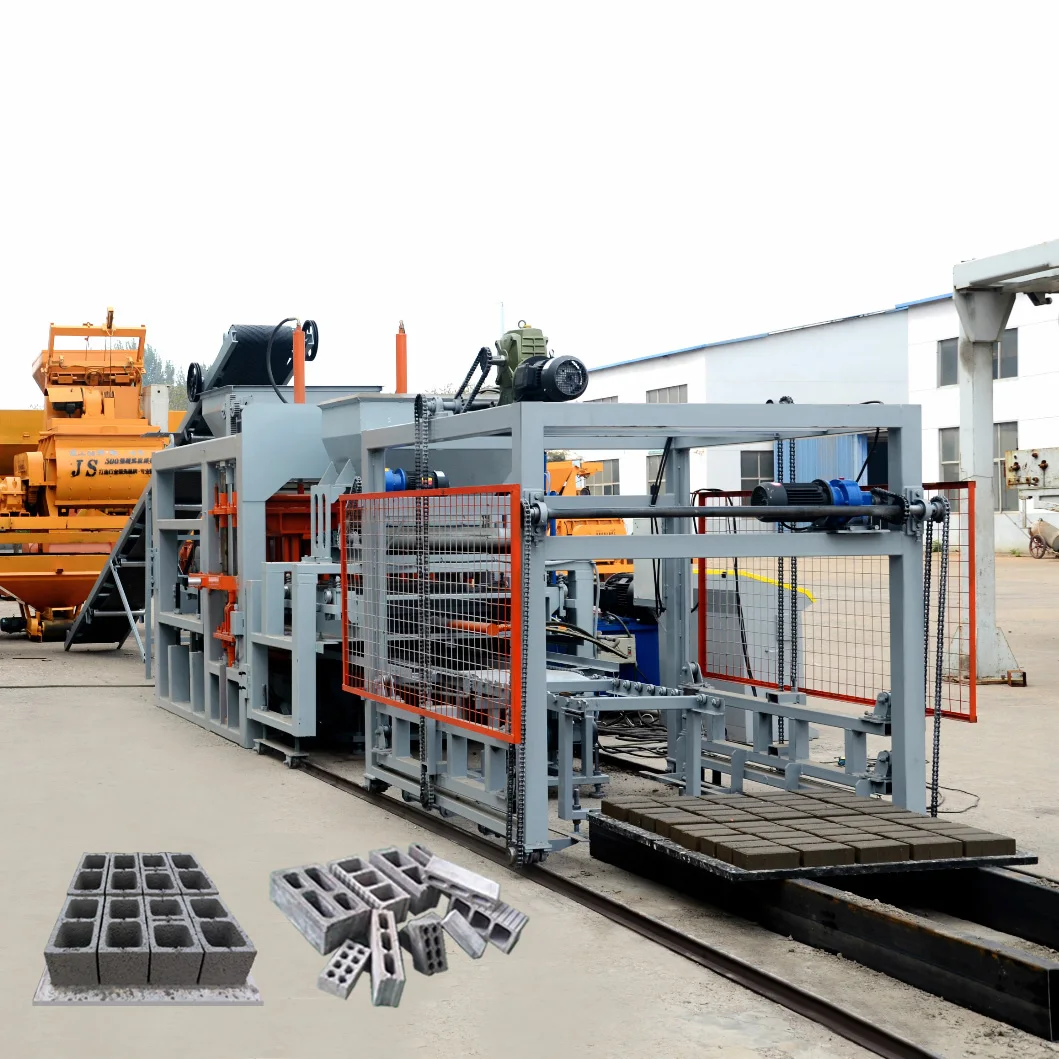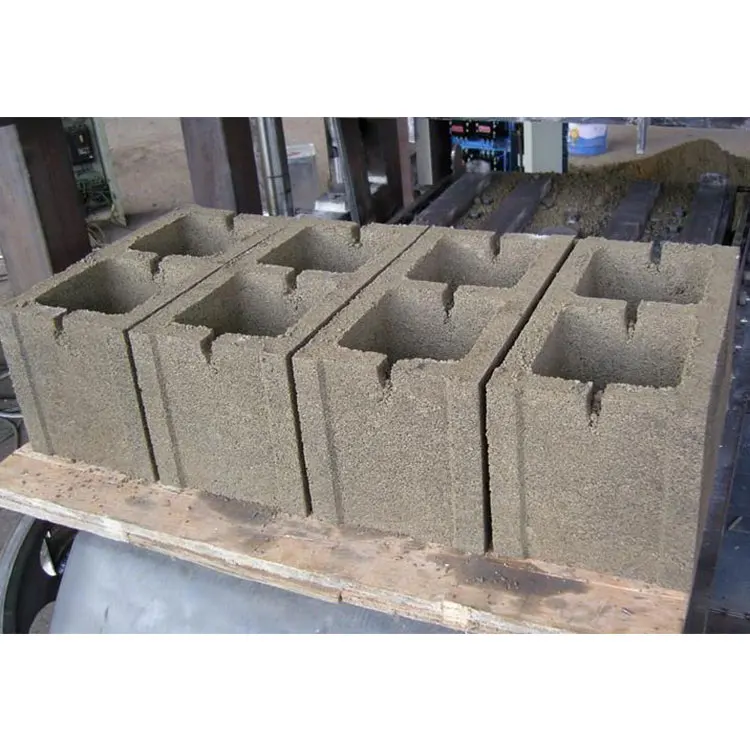

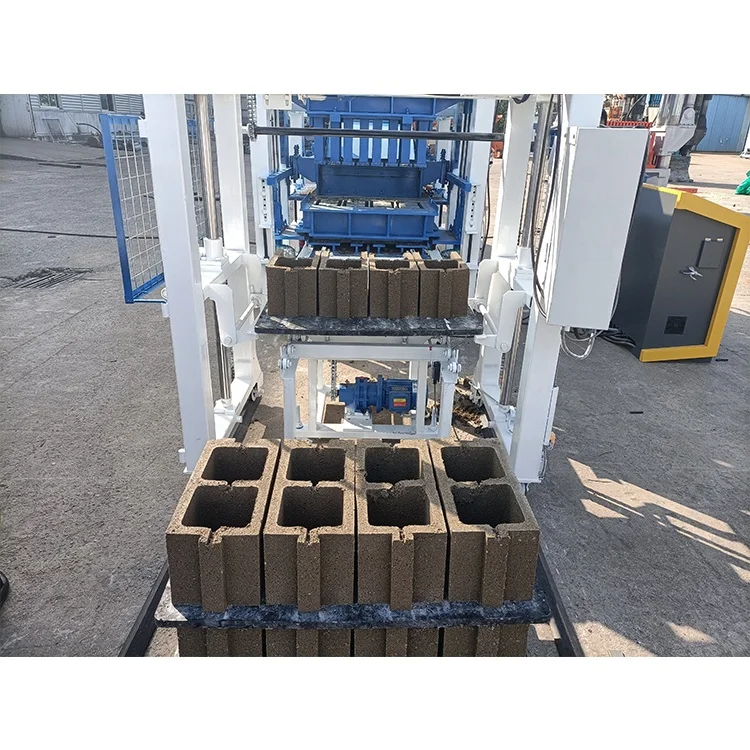
Description
Mould-Driven Sizing — every QT4-16 capacity figure we quote names the exact block format, cycle time and pallet area behind it, so daily output reflects your market’s real product mix.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-16 |
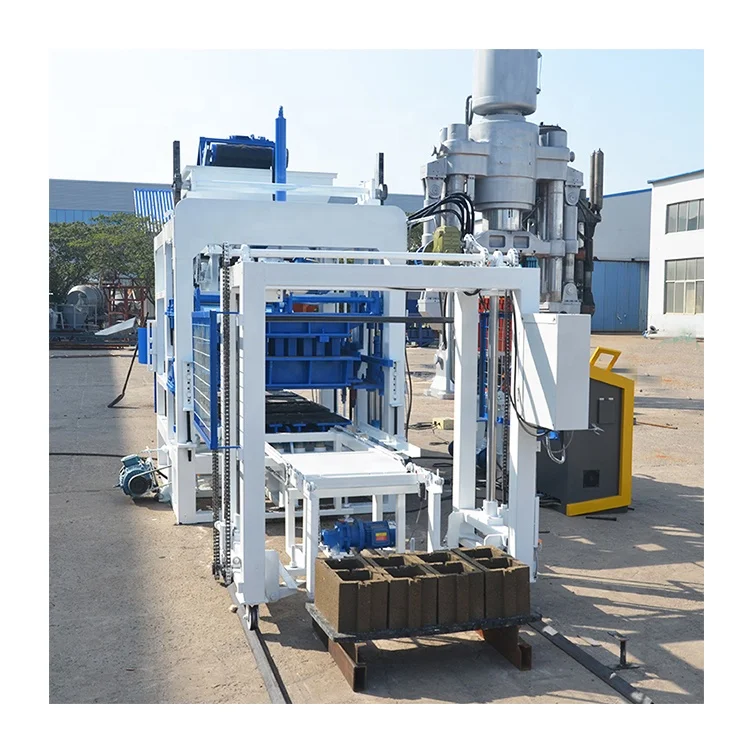
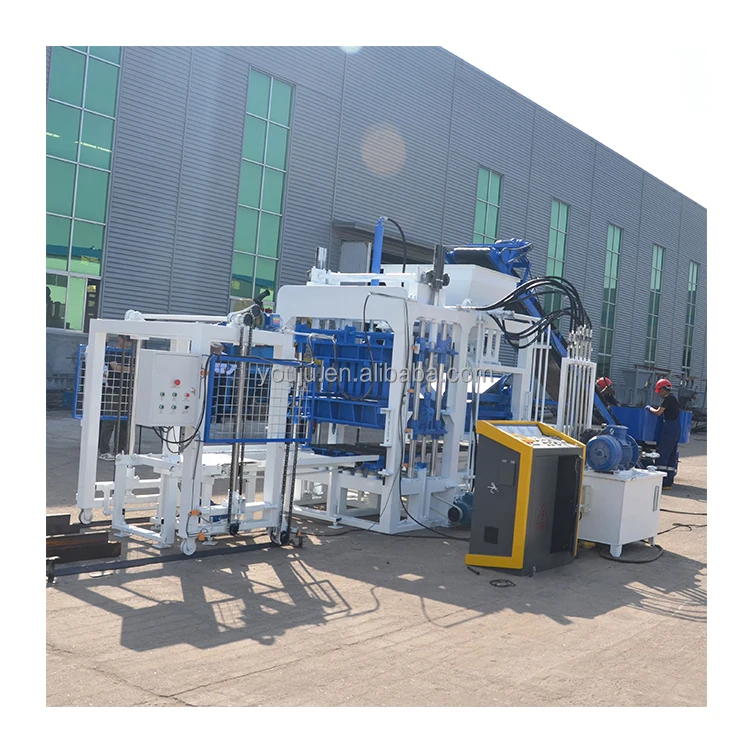
| Product Type | Automatic Hydraulic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 7400 × 1950 × 2800 mm |
| Rated Hydraulic Pressure | 21 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency Range | 2800 – 4500 r/min |
| Vibration Force | 40 kN |
| Pallet Size | 900 × 550 mm |
| Moulding Cycle | 15 – 20 s (basis not stated in source — confirm block format, material and thickness) |
| Total Machine Mass | 5 T |
| Demolding Method | Hydraulic |
| Recommended Factory Area | 600 m² |
| Control System | PLC intelligent control with HMI, logic control, malfunction diagnosis, remote control function |
| Machine Frame Material | Manganese steel (China national standard) |
| Voltage & Frequency | Configurable — confirm with buyer before production |
| PLC Display Language | Configurable — confirm with buyer before production |
Application Suitability
| Application | Material or Output |
|---|---|
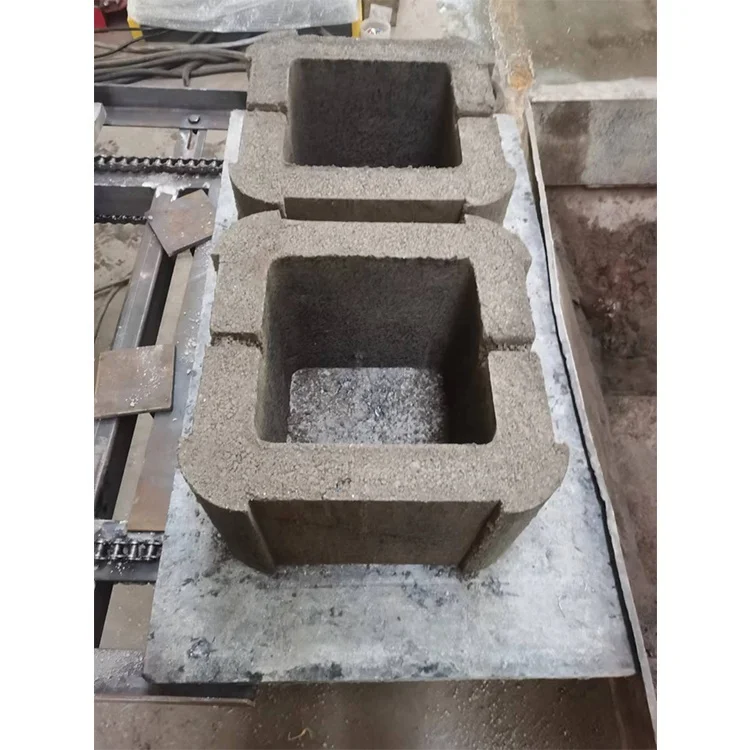
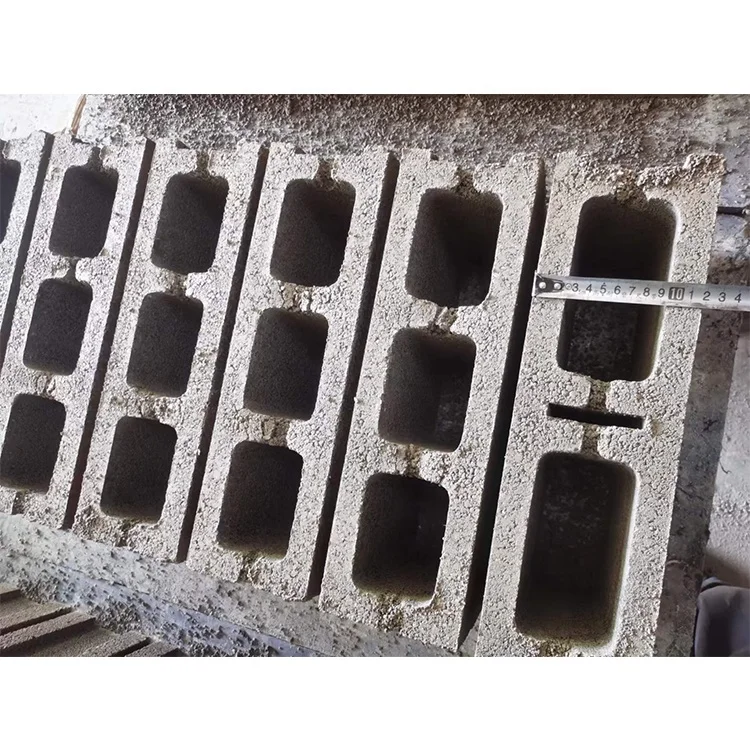
| 8-inch hollow block production | Crushed stone, sand, cement, fly ash |
| 6-inch and 4-inch hollow block production | Gravel, slag, cement blends |
| Solid load-bearing block manufacturing | Dense aggregate and cement mixes |
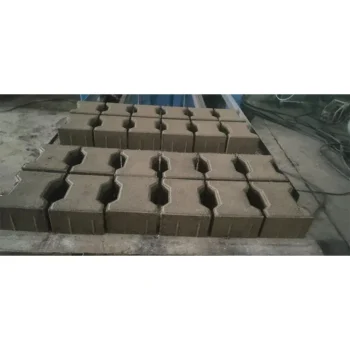
| Interlocking brick and paver runs | Colored face-mix with fine aggregate |
| Kerbstone and curb unit forming | Coarse aggregate with high cement content |
What "15–20 Seconds per Cycle" Actually Means for Your Output
A cycle time is only meaningful when tied to the block format and the mix feeding that mould.
Sellers often quote the fastest possible cycle — typically a thin paver or a small solid block — and let buyers assume the same rhythm applies to an 8-inch hollow block. On a desert-sand mix I once saw shipped to a Gulf site, the moulding cycle stretched well beyond the catalogue figure because the vibration frequency had been set for river sand. The blocks collapsed at demolding, and the crew spent half the shift scraping the press table. When you evaluate automatic block machine specifications, always ask which format and which aggregate produced the stated cycle, then verify against your own material [NEED_CITE: block cycle time versus aggregate grading standards].
Matching Vibration to Your Local Aggregate
The platform vibration system on this automatic block machine spans 2800 to 4500 r/min, and that range exists because different aggregates demand different energy inputs. Desert sand, with its rounded grains, needs a higher frequency and longer dwell to achieve interlock, while angular crushed stone compacts quickly at the lower end of the band. If the frequency is too high for a coarse mix, the fines migrate to the surface and the block core stays weak. Getting this right is the difference between passing a compressive strength test on the first batch and re-pouring an entire day’s output.
Pallet Sizing Against Your Curing Yard
A 900 × 550 mm pallet sounds like a small detail until it arrives at a site where the curing racks were welded for a different dimension. Forklift tine spacing, rack slot width and stacking height all depend on that single measurement. Before we ship any QT4-16, we ask for a drawing of the buyer’s curing area and the forklift model already on site. Changing pallet size after the machine is built means new mould bases, new rack slots and possibly a new forklift — an expense that erases the margin on the first container of blocks [NEED_CITE: pallet dimension compatibility in concrete block plants].
Reading the Pressure and Vibration Numbers Together
Twenty-one megapascals of hydraulic pressure and 40 kN of vibration force are not independent specs; they work as a pair. Pressure squeezes the mix from above while vibration settles it from below. If pressure dominates, the block surface looks dense but the core may carry air pockets. If vibration dominates, the fines rise and the bottom face turns brittle. The PLC on the QT4-16 lets the operator store separate recipes, each with its own pressure-vibration balance, so a morning run of hollow blocks and an afternoon run of pavers can each have a saved profile rather than relying on manual dial adjustments.
The Cost of Skipping the Mix-Vibration Match
I once watched a contractor in the Levant lose an entire week of production because the vibration force had been factory-set for a granite-dust mix that was unavailable locally. The blocks left the mould with micro-cracks along the webs, and every third course on the site wall had to be torn down. The fix was not a new machine but a new recipe — yet the delay pushed the masonry schedule into the rainy season, and scaffolding rental alone wiped out the profit on that building. Mis-matched vibration and aggregate is one of the most common hidden costs in block production, and it only shows up once the press is running on your floor [NEED_CITE: aggregate substitution effects on concrete block strength].
Why Procurement Conversations Start with Your Block Format
Every QT4-16 we configure begins with the buyer’s target format, local aggregate sample and required block strength, not a catalogue default. Moulds are designed to the formats the buyer’s market actually sells, including custom drawings when standard cavities do not match. Pallets, handling gear and curing racks are specified as one system with the press, so there is no mismatch on arrival. Voltage, frequency and PLC display language are locked in before production starts, preventing the commissioning delays that happen when a control panel arrives in a language the operator cannot read. Automation level is selectable, letting a buyer begin with semi-automatic pallet handling and add automatic stacking later. Factory test records are run on the buyer’s own mix sample whenever logistics allow, so the first container carries proof, not promises.
Documentation & Verification
- Line layout showing capacity calculation for each block format you intend to produce
- Mould drawing set listing cavity count and dimensional tolerances per format
- Pallet specification matched to your curing rack slot width and forklift tine spacing
- Hydraulic and electrical schematic with confirmed voltage and frequency
- Factory test record run on your aggregate sample before dispatch
- Operation and maintenance manual in your chosen PLC display language
Installation, Commissioning & Support
- Foundation plan sized to the QT4-16 footprint of 7400 × 1950 mm with anchor bolt schedule
- Dedicated power circuit confirmed for your local voltage before the control cabinet is wired
- Machine shipped in bolted sub-assemblies for container loading and reassembly on site
- First-run parameter tuning against your mix design with operator present at the PLC
- Mould change procedure training covering hydraulic clamp release and cavity alignment
- Wear parts list covering platform springs, hydraulic seals and mould liner plates
Preparing Your Inquiry
To size the QT4-16 accurately we need the block formats your market sells most, the local aggregate type and a target daily output per format. Share your site voltage and frequency, the curing area dimensions, and the forklift model you plan to use for pallet handling. If you already run a mixer or batching plant upstream, send its make and batch weight so the feed rate can be matched.
Frequently Asked Questions
Q: How does the 15–20 s moulding cycle change across block formats?
A: The stated range assumes a specific format and mix; an 8-inch hollow block typically needs a longer cycle than a thin paver because more material must settle into deeper cavities. We confirm the exact cycle per format against your aggregate before finalizing the automatic block machine specifications.
Q: How do I match vibration force to my local aggregate?
A: Send a sample of your sand or crushed stone so we can run trial pressings. Rounded desert sand usually requires higher frequency and longer dwell, while angular crushed stone compacts faster. The PLC stores separate recipes so each aggregate blend keeps its own vibration profile.
Q: What mould formats fit the QT4-16, and how fast is a changeover?
A: Standard options include 4-inch to 8-inch hollow blocks, solid blocks, pavers and interlocking bricks, with custom cavities available to buyer drawings. Changeover involves releasing the hydraulic clamps and lifting the mould cassette; actual time depends on crane access at your site.
Q: How do I confirm the pallet size works with my curing area?
A: Provide a sketch of your curing rack dimensions and the forklift model on site. We then verify that the 900 × 550 mm pallet slides into existing rack slots and that the forklift tines can span the pallet width without overhang.
Q: When must voltage and PLC language be confirmed?
A: These must be locked before the control cabinet is wired, which happens early in production. Share your site voltage, frequency and preferred display language at inquiry stage so the automatic block machine specifications sheet reflects them and commissioning is not delayed on arrival.