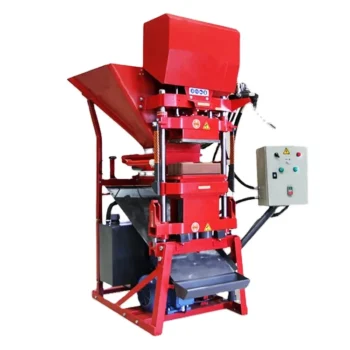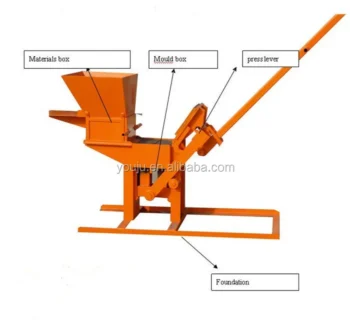
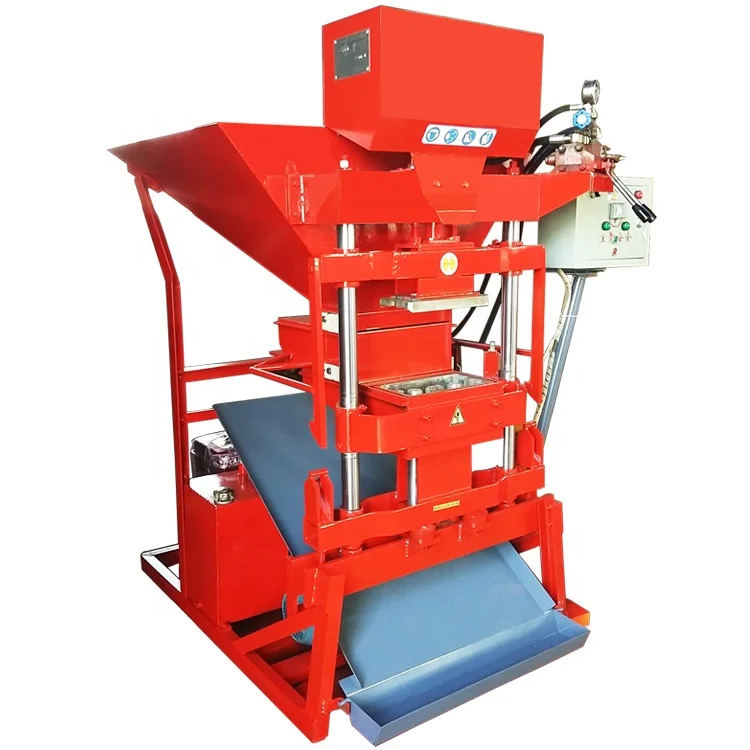
Description
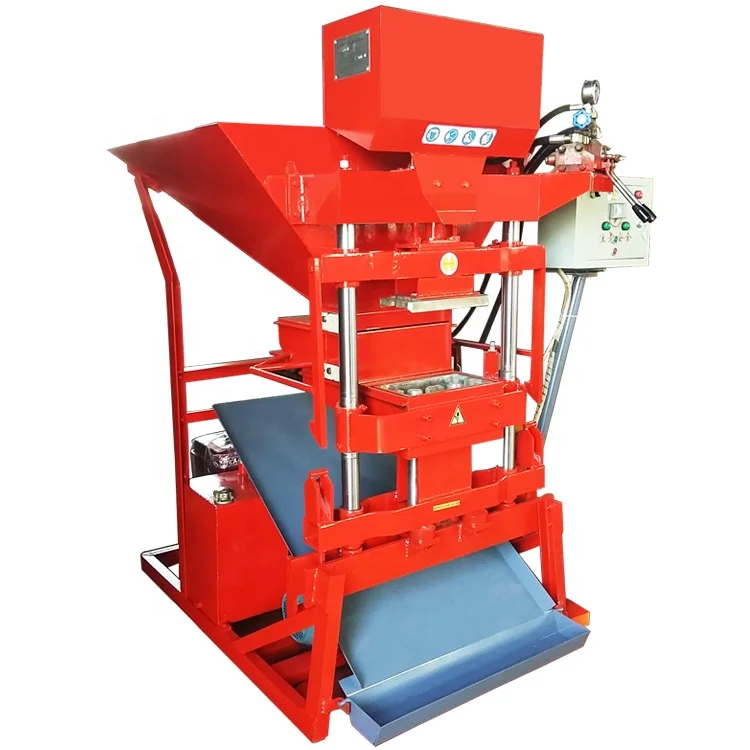
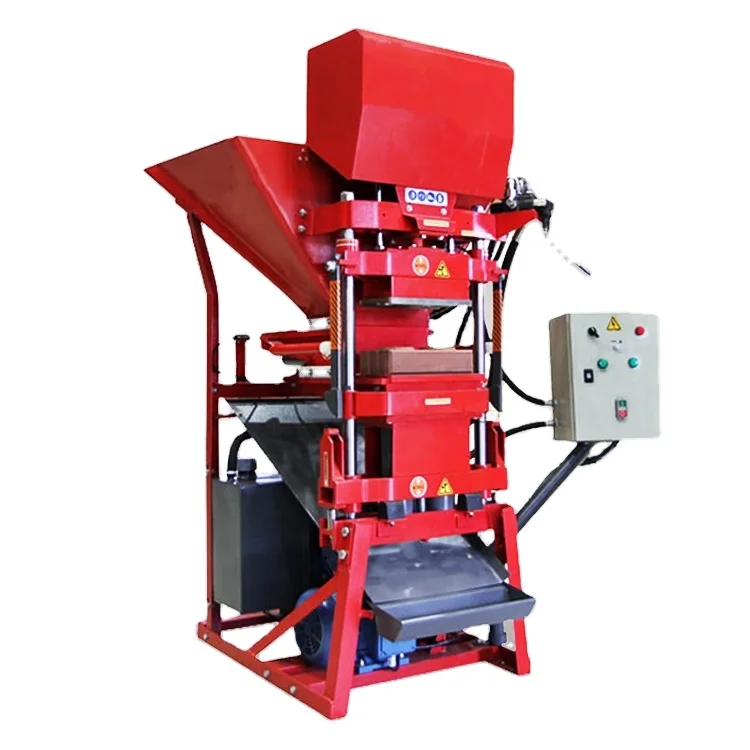
Matched mould profiles — every interlocking clay brick die is sized to your local soil behaviour, not a catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Clay Interlocking Brick Making Machine |
| Model | ECO 2700 |
| Overall Dimensions (L×W×H) | 1000×1000×1800 mm |
| Shaping Cycle | 15-20 seconds (basis to be confirmed by brick format) |
| Rated Power | 5.5 kW |
| Hydraulic Pressure | 16 MPa |
| Total Weight | 1000 KGS |
| Operation Mode | Manual / No power required for forming |
| Voltage & Frequency | 380V, 3-phase, 50Hz (customizable to local voltage) |
| Automation Level | Manual / small-sized forming machine |
| Stacking Method | Manual |
| Warranty | 1 year |
Application Suitability
| Application | Material or Output |
|---|---|
| Small-scale interlocking clay brick production | Local clay or soil with stabiliser additive |
| On-site brick making for construction contractors | Excavated site soil blended with cement or lime |
| Low-investment ecological brick plants | Laterite, red clay, or sandy loam mixed with binder |
Why "Cycles per Hour" Tells You Nothing About Your Actual Output
The cycle time printed on a nameplate assumes a brick format you may not even sell.
Many buyers discover after commissioning that the headline cycle rate was measured on a small paver, not the large interlocking profile their market demands. When the actual mould cavity is bigger and the clay mix denser, each press stroke takes longer and the daily count drops. I spent two weeks on a project in Peru where the interlocking brick machine ran at barely half its quoted throughput because the local clay held too much moisture and the operator had to wait for each brick to release cleanly from the die. Always ask which exact brick dimension the cycle figure assumes before you sign anything. [NEED_CITE: common discrepancy between quoted and actual block machine output]
Matching Mould Profile to the Brick Your Market Actually Buys
An interlocking brick only works if the tongue-and-groove geometry holds under load. The clay interlocking brick machine specifications matter less than whether the mould produces a profile local masons trust. A die cut for a 250 mm long brick will not produce a 300 mm format without a full mould swap, and every swap eats into the shift.
How Local Clay Behaviour Changes the Pressing Recipe
Not all clay presses the same way. High-plasticity soil needs a different moisture window than sandy loam, and the 16 MPa hydraulic pressure must be tuned to the mix, not left at a factory default. When the pressure is too high for a sticky mix, the brick cracks on ejection; too low and the interlocking edges crumble during handling. Sending a raw material sample before the machine ships lets the press settings be matched to your actual soil. [NEED_CITE: soil stabilisation methods for compressed earth blocks]
Reading the Specs That Actually Matter on Site
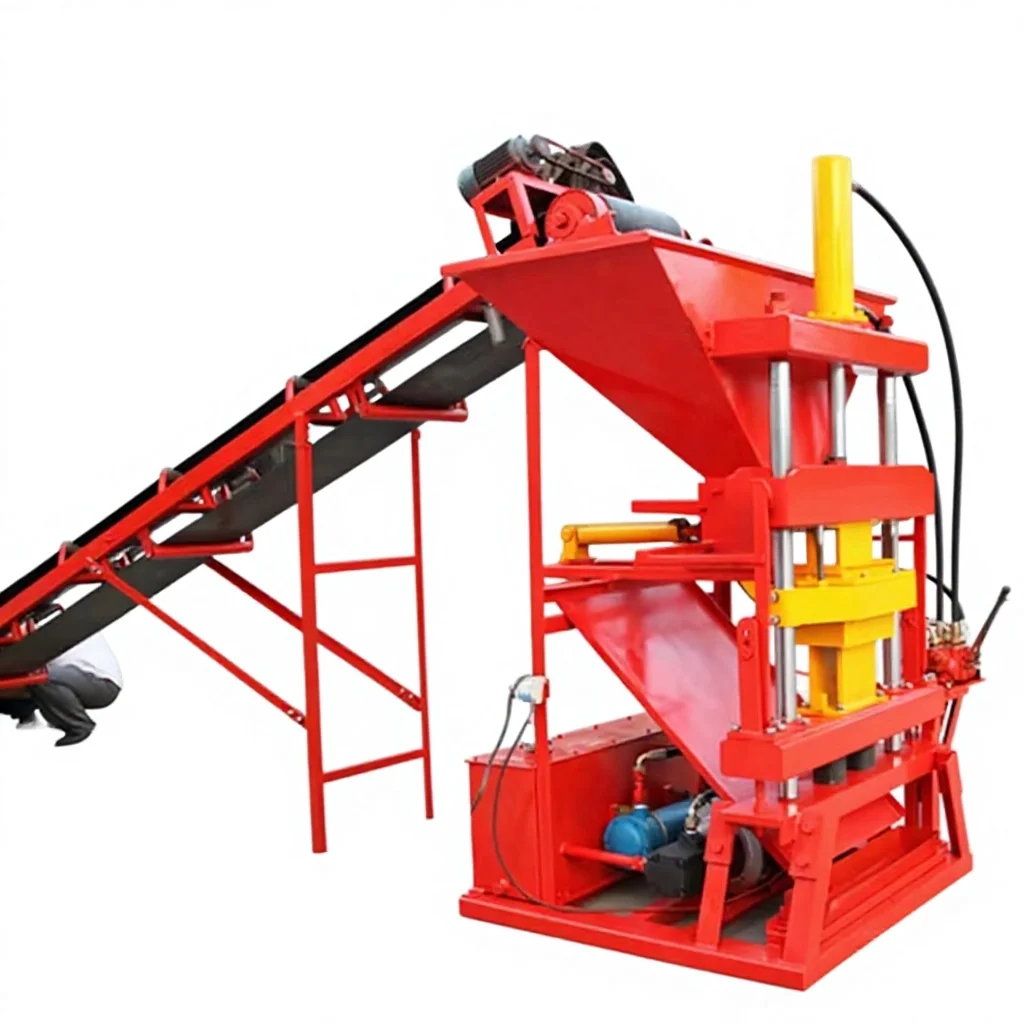
The 5.5 kW motor is sized for a manual-cycle machine that does not run a conveyor or mixer, which keeps the electrical draw low enough for a small generator set. The 1000×1000×1800 mm footprint fits inside a single standard container and can be positioned on a level concrete pad without a special foundation. Voltage is configurable, so a site running 220V three-phase in parts of Latin America will not face a transformer delay on arrival. The manual operation mode means no PLC to troubleshoot, but it also means cycle consistency depends entirely on the operator’s rhythm.
The Cost of Skipping the Material Test
When a buyer orders without sending a soil sample, the machine arrives set for a generic red clay that may bear no resemblance to the sticky laterite or silty loam on site. Bricks crack during demoulding, interlocking edges chip, and the crew blames the machine. The real problem is a pressure and moisture mismatch that could have been corrected in a single factory trial. [NEED_CITE: importance of soil testing for compressed interlocking brick production]
What You Get When the Line Is Specified as One System
The ECO 2700 is configured around the interlocking profile you confirm, not pulled from a warehouse and paired with whatever mould happens to be in stock. The hydraulic pressure, mould cavity, and manual stroke timing are set together so the first brick off the press matches the sample you approved. Mould drawings are shared before production so you can verify the tongue-and-groove dimensions against your market standard. Documentation ships with the machine, including a factory test record run on a material as close to yours as available. Support after arrival covers the initial pressing sessions so the operator learns the moisture window by feel, not by scrapping a hundred bricks.
Documentation & Verification
- Line layout showing ECO 2700 placement, curing area, and material feed zone
- Mould drawing confirming the exact interlocking profile and brick dimensions
- Voltage and frequency confirmation sheet signed before production begins
- Factory test record using target clay or soil mix where available
- Operation manual with moisture-range guidance for common soil types
- Packing photographs and customs documentation for smooth clearance
Installation, Commissioning & Support
- Level concrete pad approximately 1.5×1.5 m is sufficient for the 1000×1000 mm base footprint
- Dedicated 3-phase circuit matching confirmed voltage and frequency required before energising the 5.5 kW motor
- Machine ships partially assembled; hydraulic lines and lever mechanism connected on site
- First-run pressing supervised remotely or via guide to dial in clay moisture and stroke timing
- Operator trained on mould release technique to prevent interlocking edge damage
- Wear parts list covering hydraulic seals and mould liner included at dispatch
What We Need from You to Size This Correctly
Send a representative sample of the clay or soil you plan to press, along with the interlocking brick dimensions your market expects. Confirm the three-phase voltage and frequency available at your site, and let us know whether you need the control interface in a language other than English. If you already run a mixer or curing racks, share their specifications so the ECO 2700 can be positioned without bottlenecking the rest of your workflow.
Frequently Asked Questions
Q: What interlocking brick formats can the ECO 2700 produce, and what is the cycle time per format?
A: The machine accepts custom moulds for various interlocking profiles. The 15-20 second shaping cycle is a general range; actual time depends on brick size, clay moisture, and operator pace. Confirm your target format so the cycle can be measured on the exact mould before shipment.
Q: Can the machine handle my local clay or soil, and how is the mix matched to the 16 MPa pressure?
A: Yes, provided a raw material sample is tested beforehand. The hydraulic pressure is adjusted to suit the density and plasticity of your specific mix, preventing edge crumbling or ejection cracking. A factory trial on your material is the most reliable way to confirm compatibility.
Q: Which voltage and frequency options are available, and is the control interface in my language?
A: The standard configuration is 380V three-phase 50Hz, but voltage is customizable to match your local grid. Since the ECO 2700 operates manually without a PLC screen, language is mainly relevant for the operation manual, which can be supplied in your preferred language on request.
Q: What mould change procedure is required when switching between interlocking profiles?
A: Mould change involves unbolting the current die from the press frame and fitting the replacement. The process is manual and typically takes a portion of a shift, so most small plants dedicate the machine to one format per production run rather than swapping daily.
Q: What supporting equipment do I need alongside the ECO 2700?
A: At minimum you need a soil-crushing or screening step, a manual or powered mixer for stabiliser blending, and a flat curing area with weather cover. Stacking and handling are done by hand given the manual operation mode of this machine.