
Description
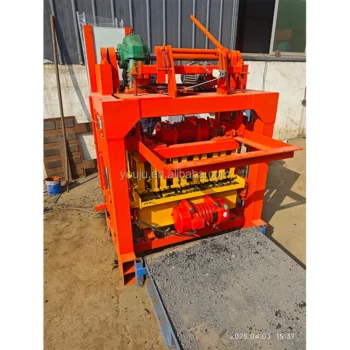
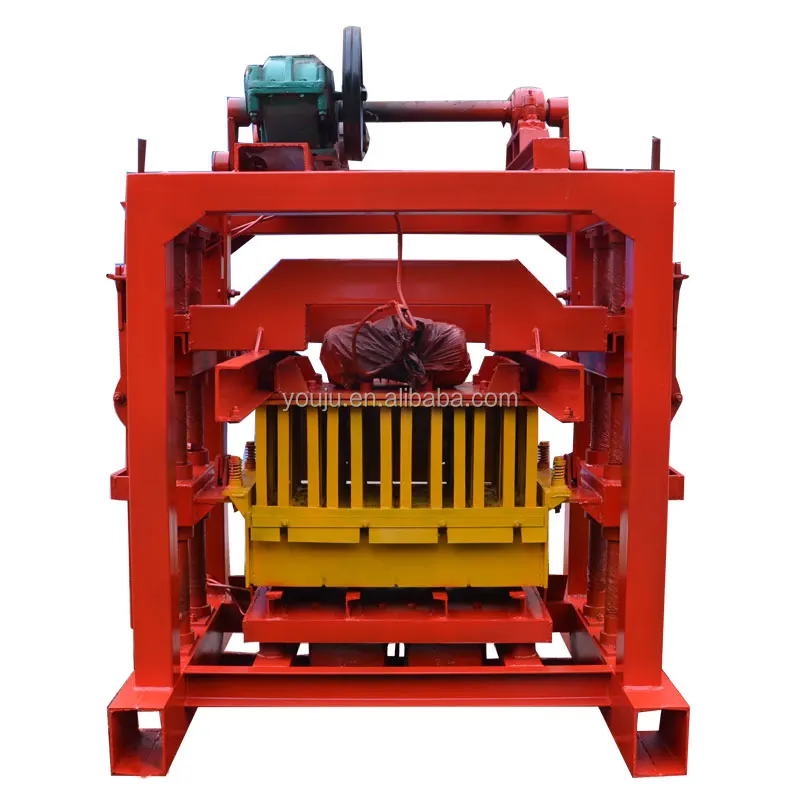
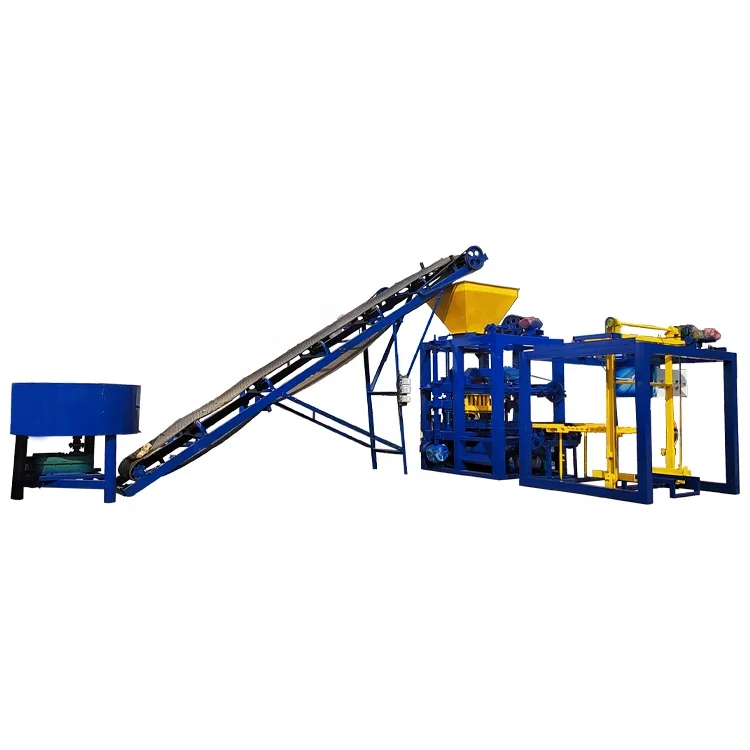
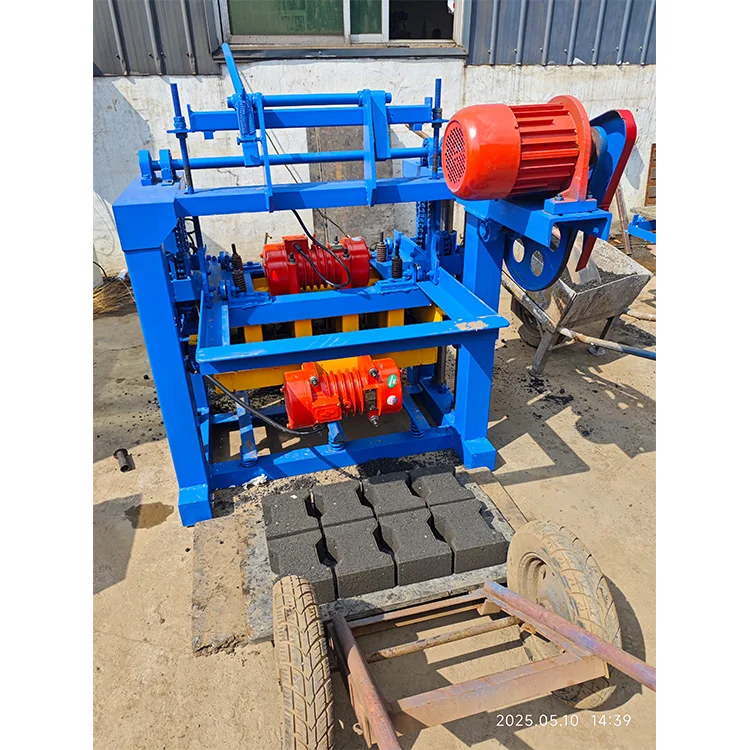
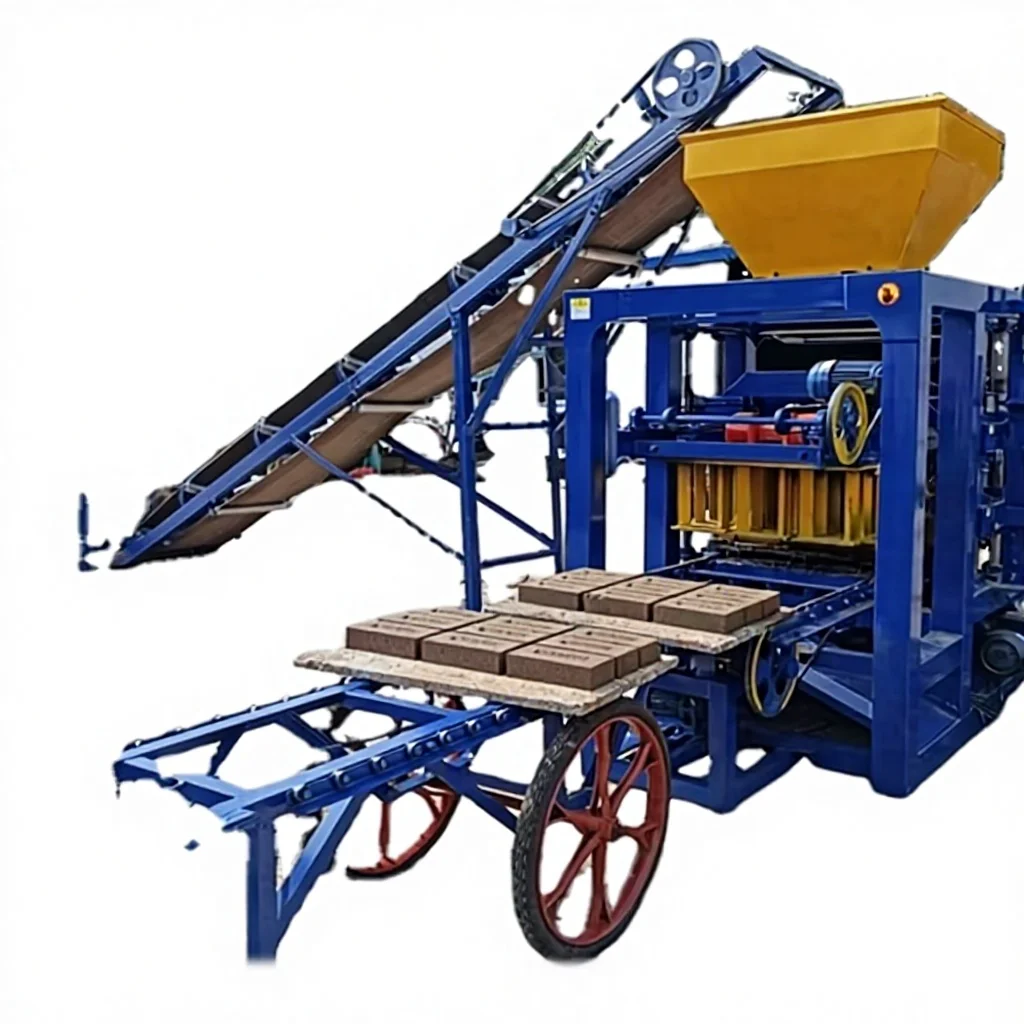
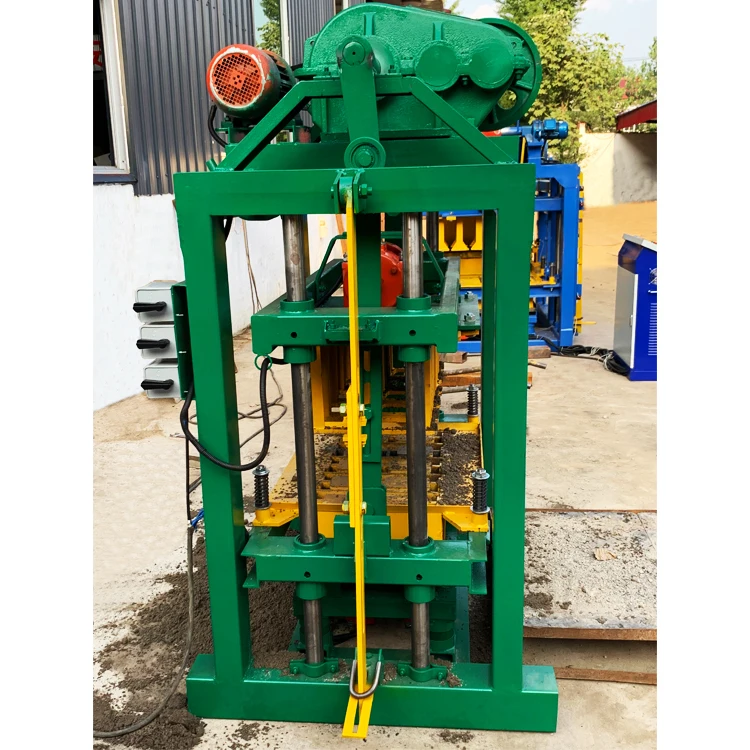
Mould and Machine Matched — The QTJ4-40 configuration starts with the block format your market actually buys, not a default catalogue setting, so cycle time and output hold up once local aggregate enters the mixer.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-40 |
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 1350×1460×1800 mm |
| Machine Weight | 1.2 T |
| Machine Power | 10.4 kW |
| Voltage & Frequency | Configurable to buyer’s local supply (confirm before production) |
| Molding Cycle | 40 s |
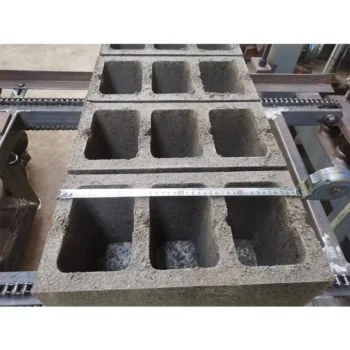
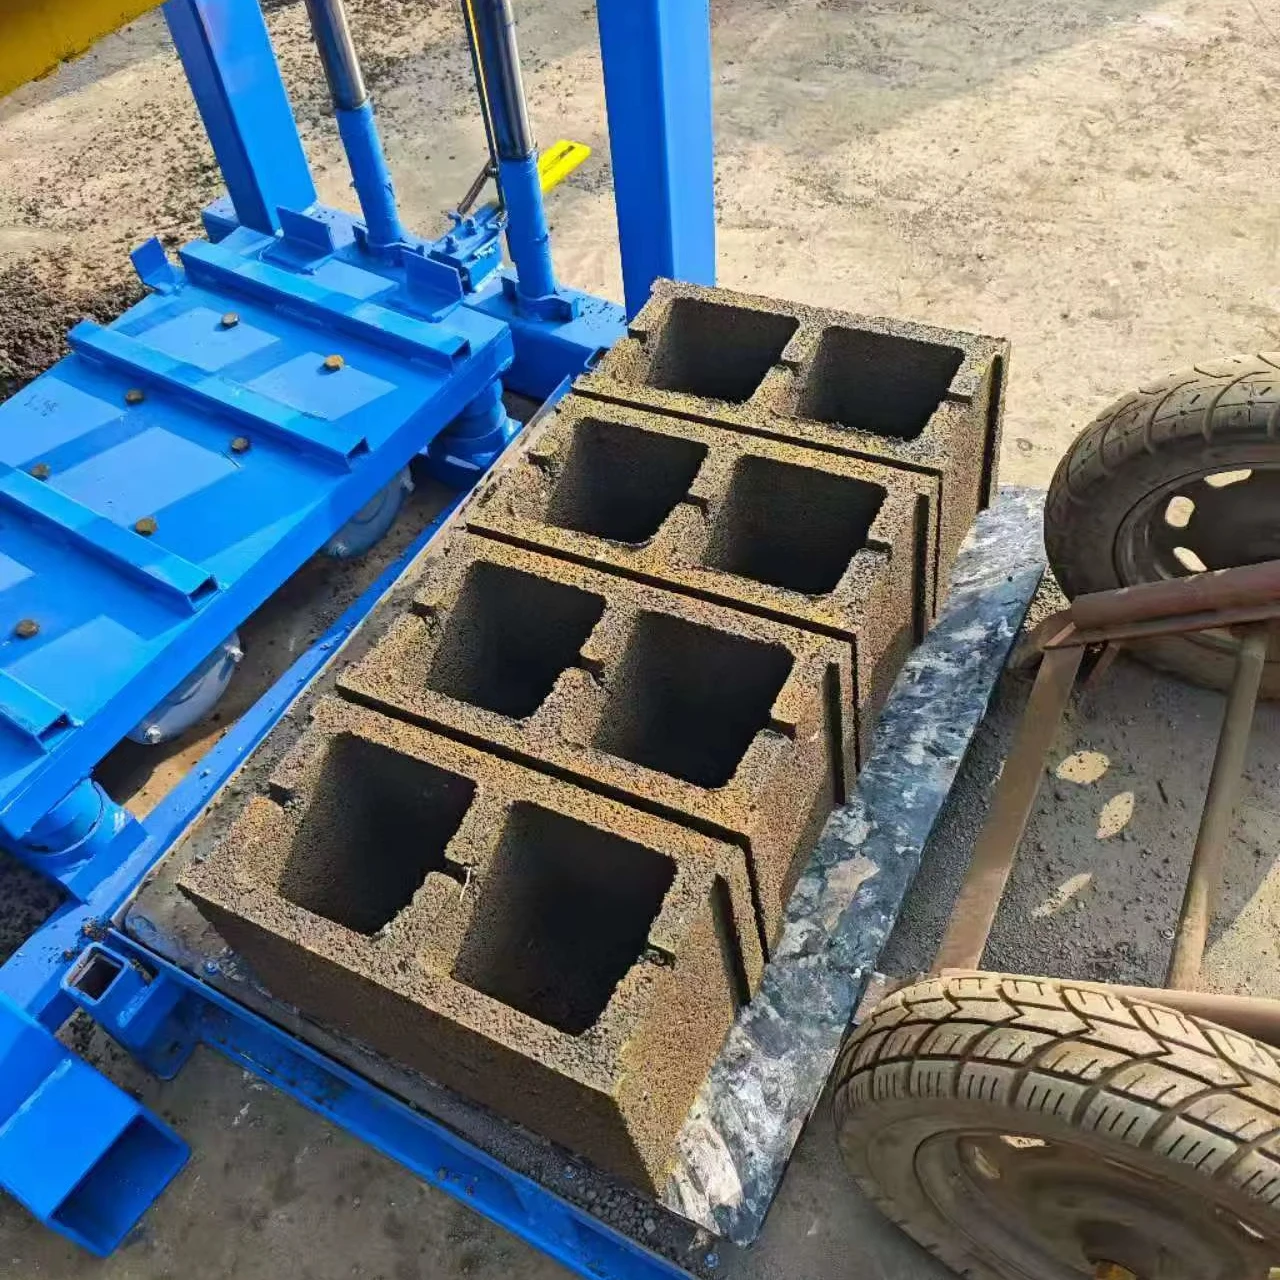
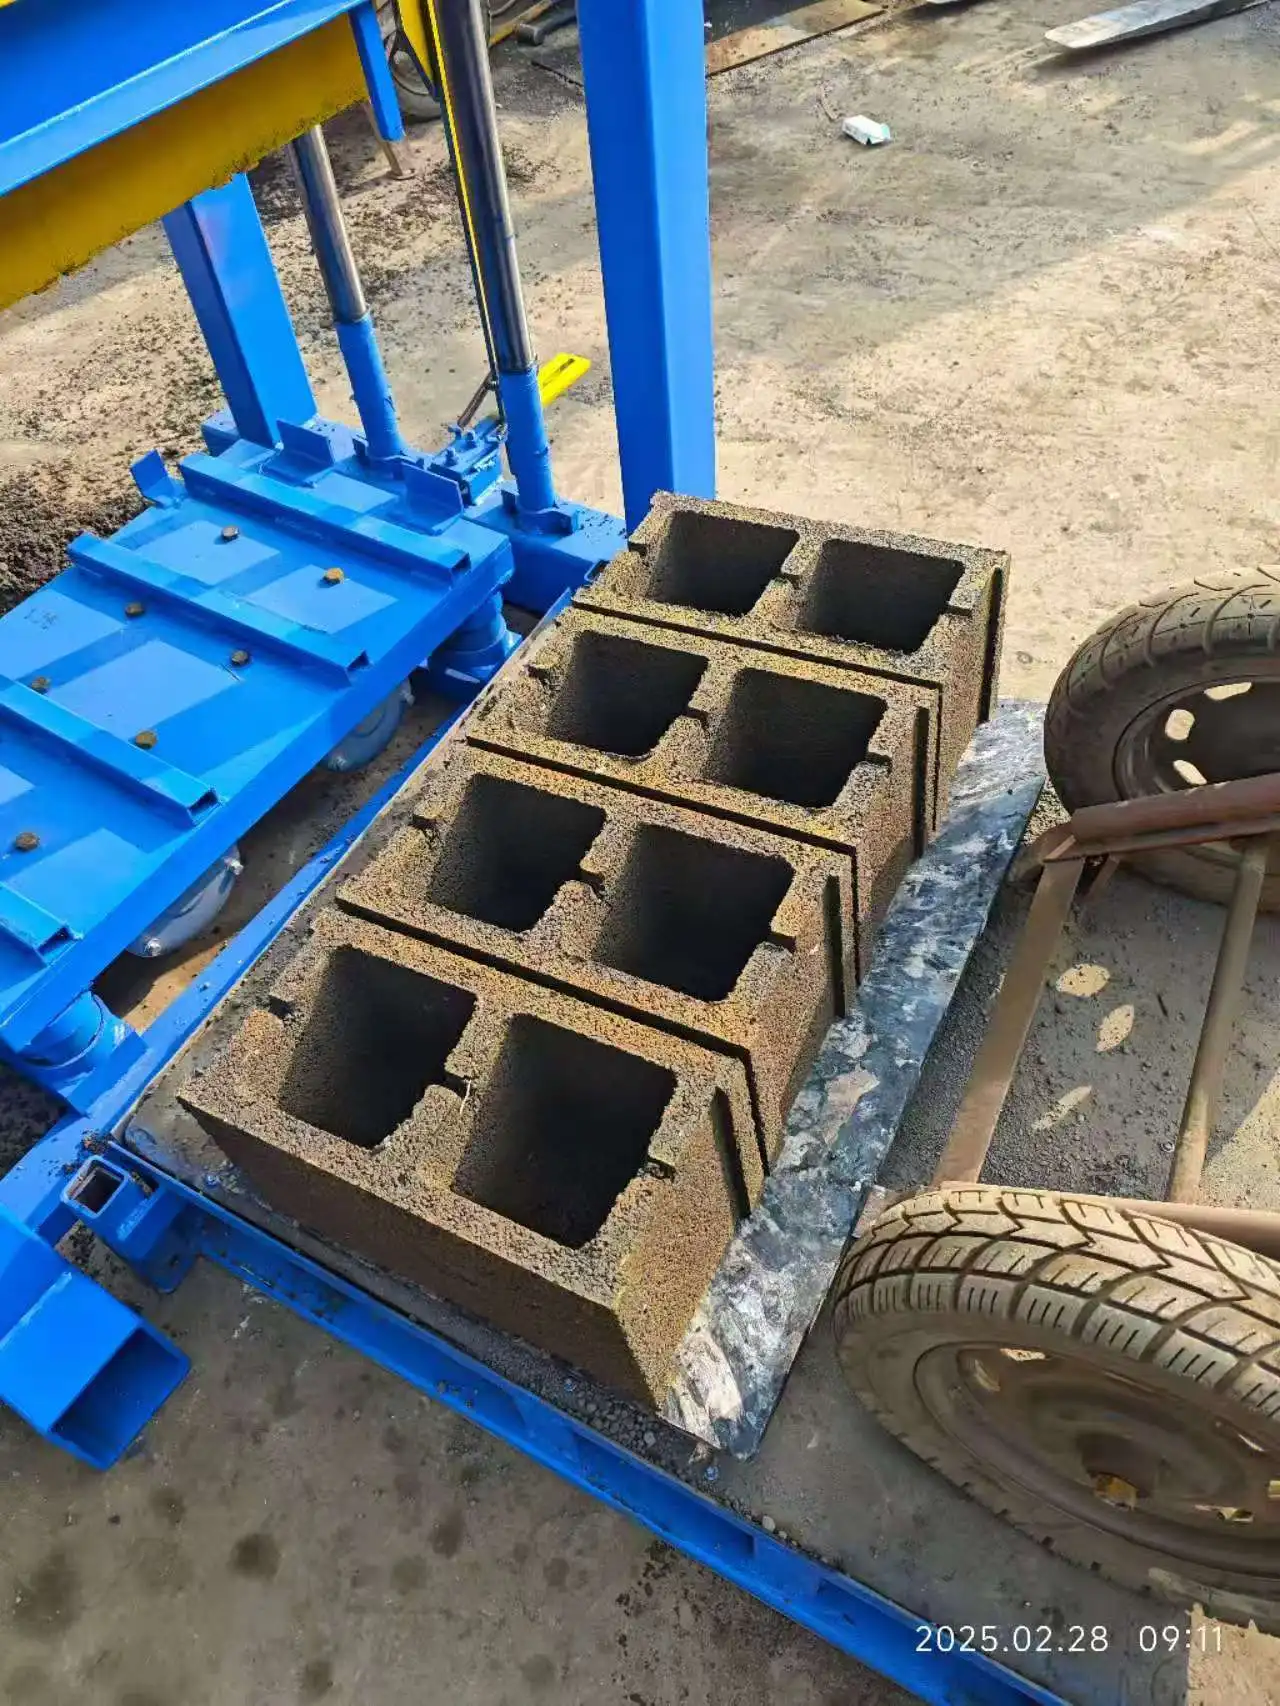
| Output — Hollow 400×200×200 mm (4 pcs/mould) | 360 pcs/h, 2,880 pcs/day (basis: 8-hour shift) |
| Output — Hollow 400×150×200 mm (5 pcs/mould) | 450 pcs/h, 3,600 pcs/day (basis: 8-hour shift) |
| Output — Solid 225×112.5×60 mm (9 pcs/mould) | 800 pcs/h, 6,400 pcs/day (basis: 8-hour shift) |
| Pallet Size | 850×450×20 mm |
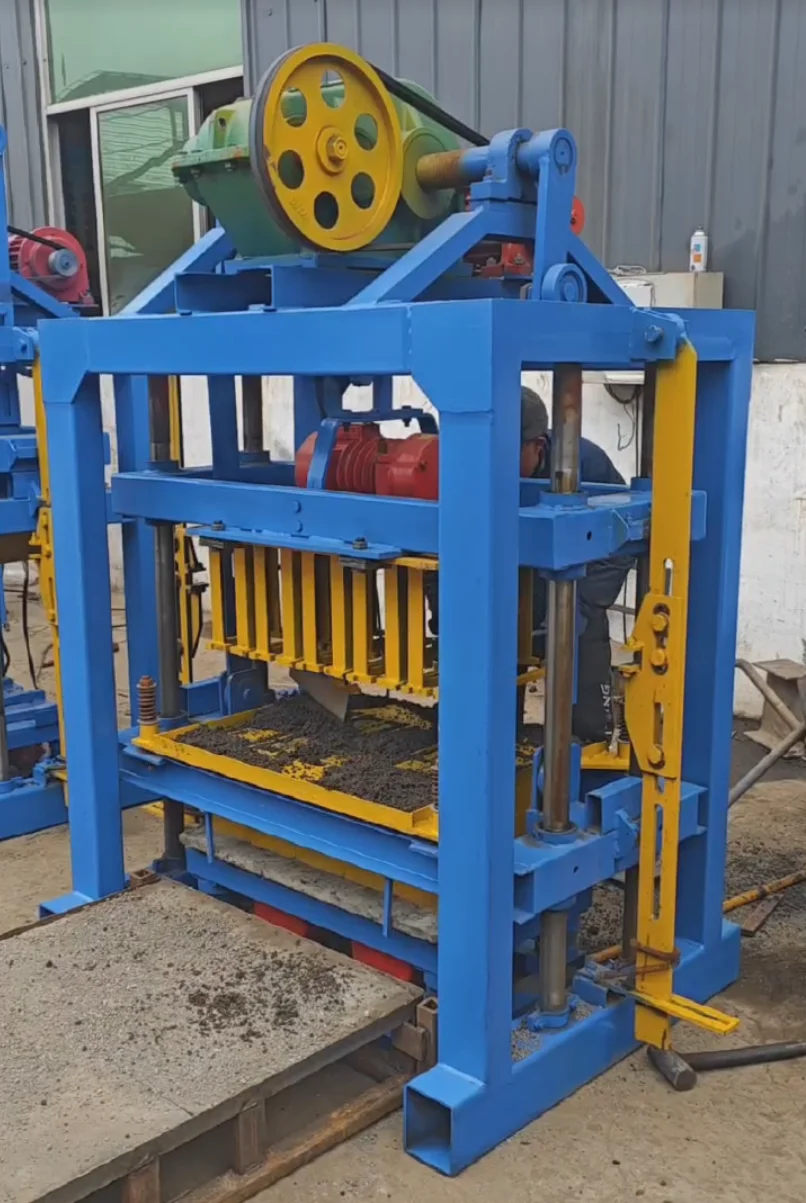
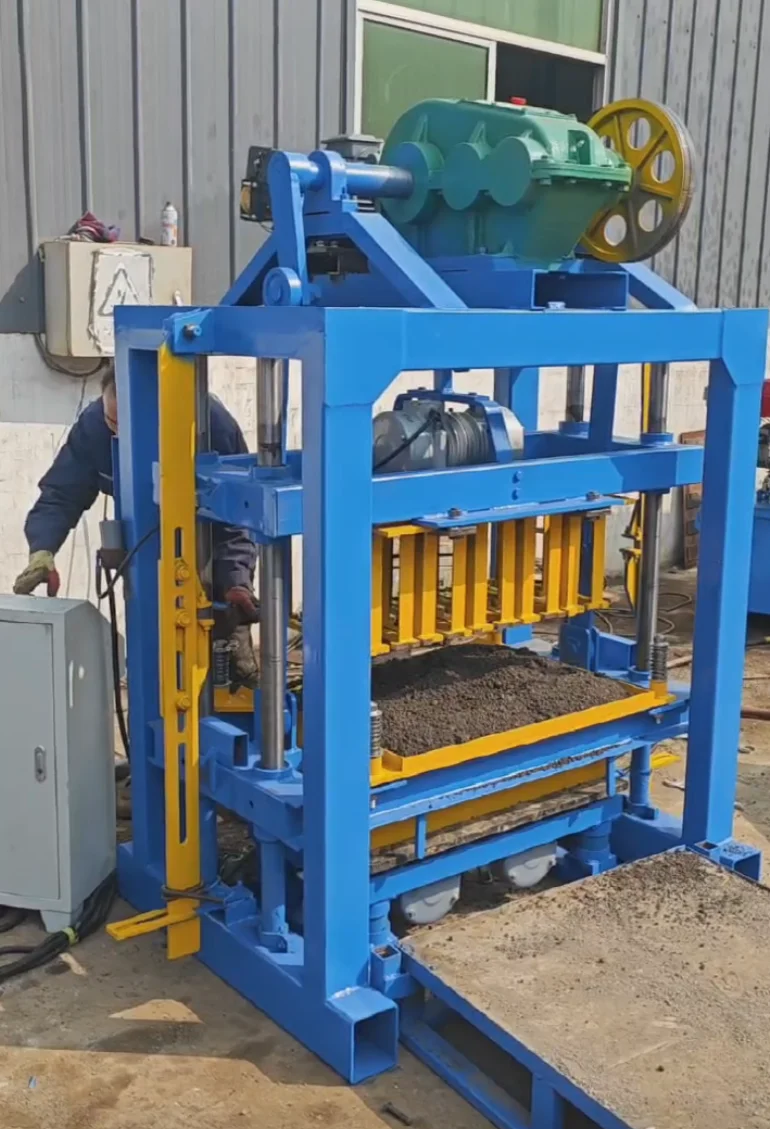
| Vibration System | Bed mould vertical vibration + upper mould compression vibration |
| Automation Level | Semi-automatic (manual pallet handling) |
| Mould Compatibility | Hollow, solid, paver blocks (8″, 6″, 5″, 4″; custom sizes on request) |
| Raw Materials | Concrete, sand, cement, fly ash, lime, gypsum |
| Supporting Equipment Required | Mixer, host machine, block mould, pallets (mixer and pallets optional if sourced locally) |
| Hydraulic Pressure | Source value — verify before quotation |
| Vibration Force | Source value — verify before quotation |
| Mould Change Time | Source value — verify before quotation |
| Certification | Source value — verify (CE or other applicable standard) |
| Control System | Source value — verify (PLC / relay / manual) |
Application Suitability
| Application | Material or Output |
|---|---|
| Small block plant producing hollow blocks for wall construction | Crushed stone, sand, cement — 400×200×200 mm or 400×150×200 mm formats |
| On-site block production for building contractors | Local aggregate and cement — hollow and solid formats to match project specs |
| First-time block producer entering the market | Standard concrete mix — solid blocks 225×112.5×60 mm or pavers |
| Existing plant adding paver formats to product range | Concrete with fine aggregate — interlocking and rectangular paver moulds |
| Fly ash brick production using industrial by-products | Fly ash, lime, gypsum, sand — solid brick formats |
What "Pieces per Hour" Leaves Out When Choosing a Semi-Automatic Concrete Block Machine
Every capacity number on this page names the exact block format, mould cavity count and cycle time it was measured against.
I once watched a buyer in the Philippines sign for a machine quoted at a single output figure. When his crew switched from 6-inch hollow to solid pavers, the real throughput dropped noticeably because the cycle time and mould cavity count were never matched to that format. The semi-automatic concrete block machine specifications you see here break output into three distinct reference formats so there is no guesswork. Buyers who skip this step often discover on the first production week that their daily target was calculated on a block they do not even sell [NEED_CITE: capacity calculation methods in block making machinery].
How the 40-Second Molding Cycle Translates to Your Daily Target
The QTJ4-40 completes one press cycle in 40 seconds, which sets the ceiling for every format the machine produces. With the 400×200×200 mm hollow mould holding four cavities, that cycle rate yields 360 blocks per hour. Switch to the five-cavity 400×150×200 mm mould and hourly output moves to 450 pieces. The semi-automatic concrete block machine specifications change with each format — not because the machine behaves differently, but because the mould geometry determines how many blocks land on each pallet.
Dual Vibration and What It Means for Block Density
The QTJ4-40 pairs vertical vibration under the bed mould with compression vibration from the upper mould head. This two-axis approach forces the concrete mix into every corner of the cavity while compacting from above, which is critical when your local aggregate has irregular particle shapes. I spent four days in an Indonesian plant where volcanic aggregate kept producing hollow blocks with weak corners on a single-axis machine. Once we adjusted the vibration balance on a dual-system press, the density readings evened out across the entire block. That kind of tuning is only possible when both vibration axes are independently present [NEED_CITE: vibration system effects on concrete block compressive strength].
Reading the Specs That Actually Matter on the Shop Floor
The 850×450×20 mm pallet size defines how much curing floor space you need and whether your existing forklift can handle loaded pallet stacks. The 10.4 kW total power draw tells your electrician the circuit rating required — this is a machine that runs on a standard industrial three-phase supply, not a dedicated high-capacity transformer. The 1.2 T machine weight means the QTJ4-40 sits on a level concrete pad without a special foundation, which matters for contractors who need to relocate the press between job sites. Mould compatibility covers common hollow, solid and paver sizes, and custom mould drawings can be produced to buyer dimensions so you can manufacture the exact format your local building code demands.
The Cost of Skipping Format-Level Configuration
Ordering a block press without confirming which mould ships with it is one of the most common mistakes I see in this equipment class. The machine arrives, the crew opens the crate, and the mould inside is for a block the buyer’s market does not purchase. A replacement mould then takes weeks to fabricate and ship, while the press sits idle and the project deadline passes. Equally costly is arriving on site to find the voltage does not match the local grid — commissioning stalls until a transformer is sourced [NEED_CITE: voltage mismatch issues in exported machinery commissioning].
Why Source the QTJ4-40 From a Single-System Supplier
Block machinery is the only product line here, so the press, mould, pallet and handling equipment are specified together rather than assembled from separate vendors. The configuration is set against your actual mix design and local aggregate, not a generic default. Mould design covers the formats your market sells, with custom drawings available when standard sizes do not match. Automation level is selectable — a buyer can begin with manual pallet handling on the QTJ4-40 and add automated pallet feeding later. Installation support includes on-site commissioning and operator training so your crew is producing acceptable blocks before the technician leaves.
Documentation & Verification
- Line layout drawing with capacity calculation stated per block format
- Mould drawing and format list confirming cavity count and block dimensions
- Pallet specification matched to your curing area and handling equipment
- Voltage, frequency and control language confirmation sheet before production
- Factory test record run on your target block format before dispatch
- Operation and maintenance manual with wear parts and mould replacement list
Installation, Commissioning & Support
- Level concrete pad required; 1.2 T machine weight eliminates heavy foundation work
- Three-phase power circuit rated for 10.4 kW confirmed before shipment
- Machine ships partially assembled; on-site setup covers mould alignment and vibration tuning
- First production run supervised to match local aggregate and mix proportions
- Operator training covers mould change procedure and daily maintenance checks
- Wear parts list and mould catalogue provided for ongoing replacement planning
What to Prepare Before Requesting a Quotation
Send the block formats your market sells — dimensions, solid or hollow, and any local standard references. Include your target daily output and the number of operating hours you plan per shift. Confirm the local voltage, frequency and the control panel language your operators need. If you already have a mixer or pallets in house, list their specifications so the line can be configured around existing equipment.
Frequently Asked Questions
Q: How is output capacity calculated, and which block format does each figure assume?
A: Each output figure on this page is tied to a specific block format, mould cavity count and the 40-second molding cycle. For example, 360 pieces per hour is based on the 400×200×200 mm hollow block with four cavities per mould. Different formats produce different hourly rates because the number of blocks per press stroke changes.
Q: What pallet size does the QTJ4-40 use, and can I use locally sourced wooden pallets?
A: The machine runs on 850×450×20 mm pallets. Locally sourced wooden pallets are accepted as long as they match this dimension and can withstand repeated vibration cycles without splitting. Fiberglass pallets are also available and typically last longer under continuous production conditions.
Q: Which block formats can this machine produce, and how is a mould change handled?
A: The QTJ4-40 produces hollow blocks in 8-inch, 6-inch, 5-inch and 4-inch widths, plus solid blocks and pavers. Custom sizes are available on request. Mould change involves unbolting the current mould set, lifting it off the vibration table and securing the replacement — a procedure covered during operator training.
Q: How do I confirm voltage, frequency and control language before shipment?
A: Provide your local electrical standard and preferred panel language during the inquiry stage. A confirmation sheet listing voltage, frequency and language is signed off before production begins, so the control system matches your site conditions when the machine arrives.
Q: What supporting equipment is required, and what can I source locally?
A: The line needs a mixer, the host machine, block moulds and pallets. If you already own a concrete mixer, it can be integrated into the setup. Pallets can be sourced locally in wood or ordered in fiberglass. The quotation specifies exactly which items are included and which the buyer supplies.